fajsdfjash ddsa dsa as sa sad sda sadfjsadjfl jsadjk fjasdlkfjaskdfdklsaj klf
jsadj
asjdklj falsdjf
jaklj
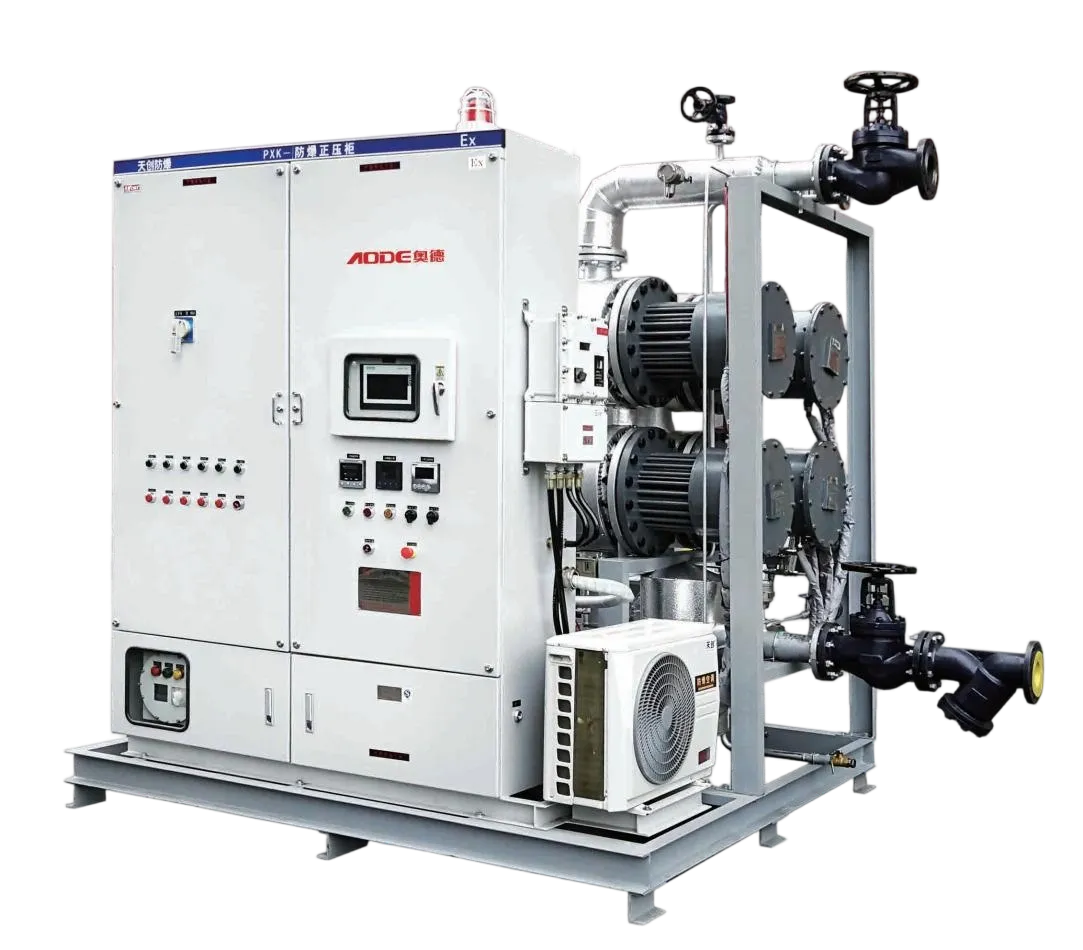
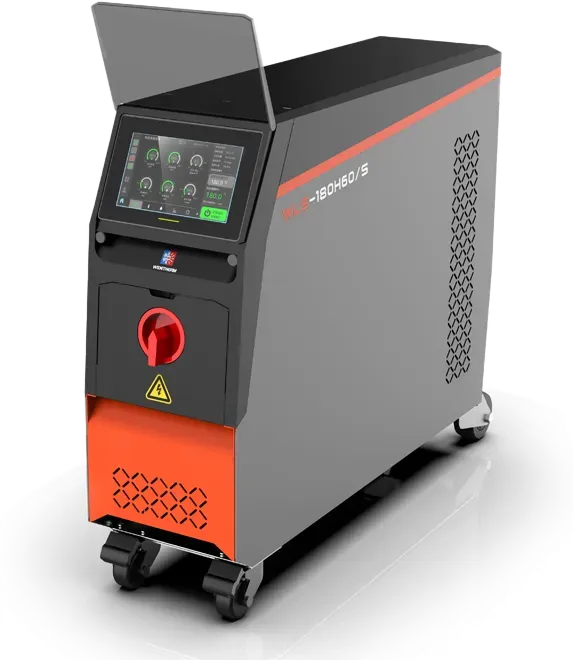
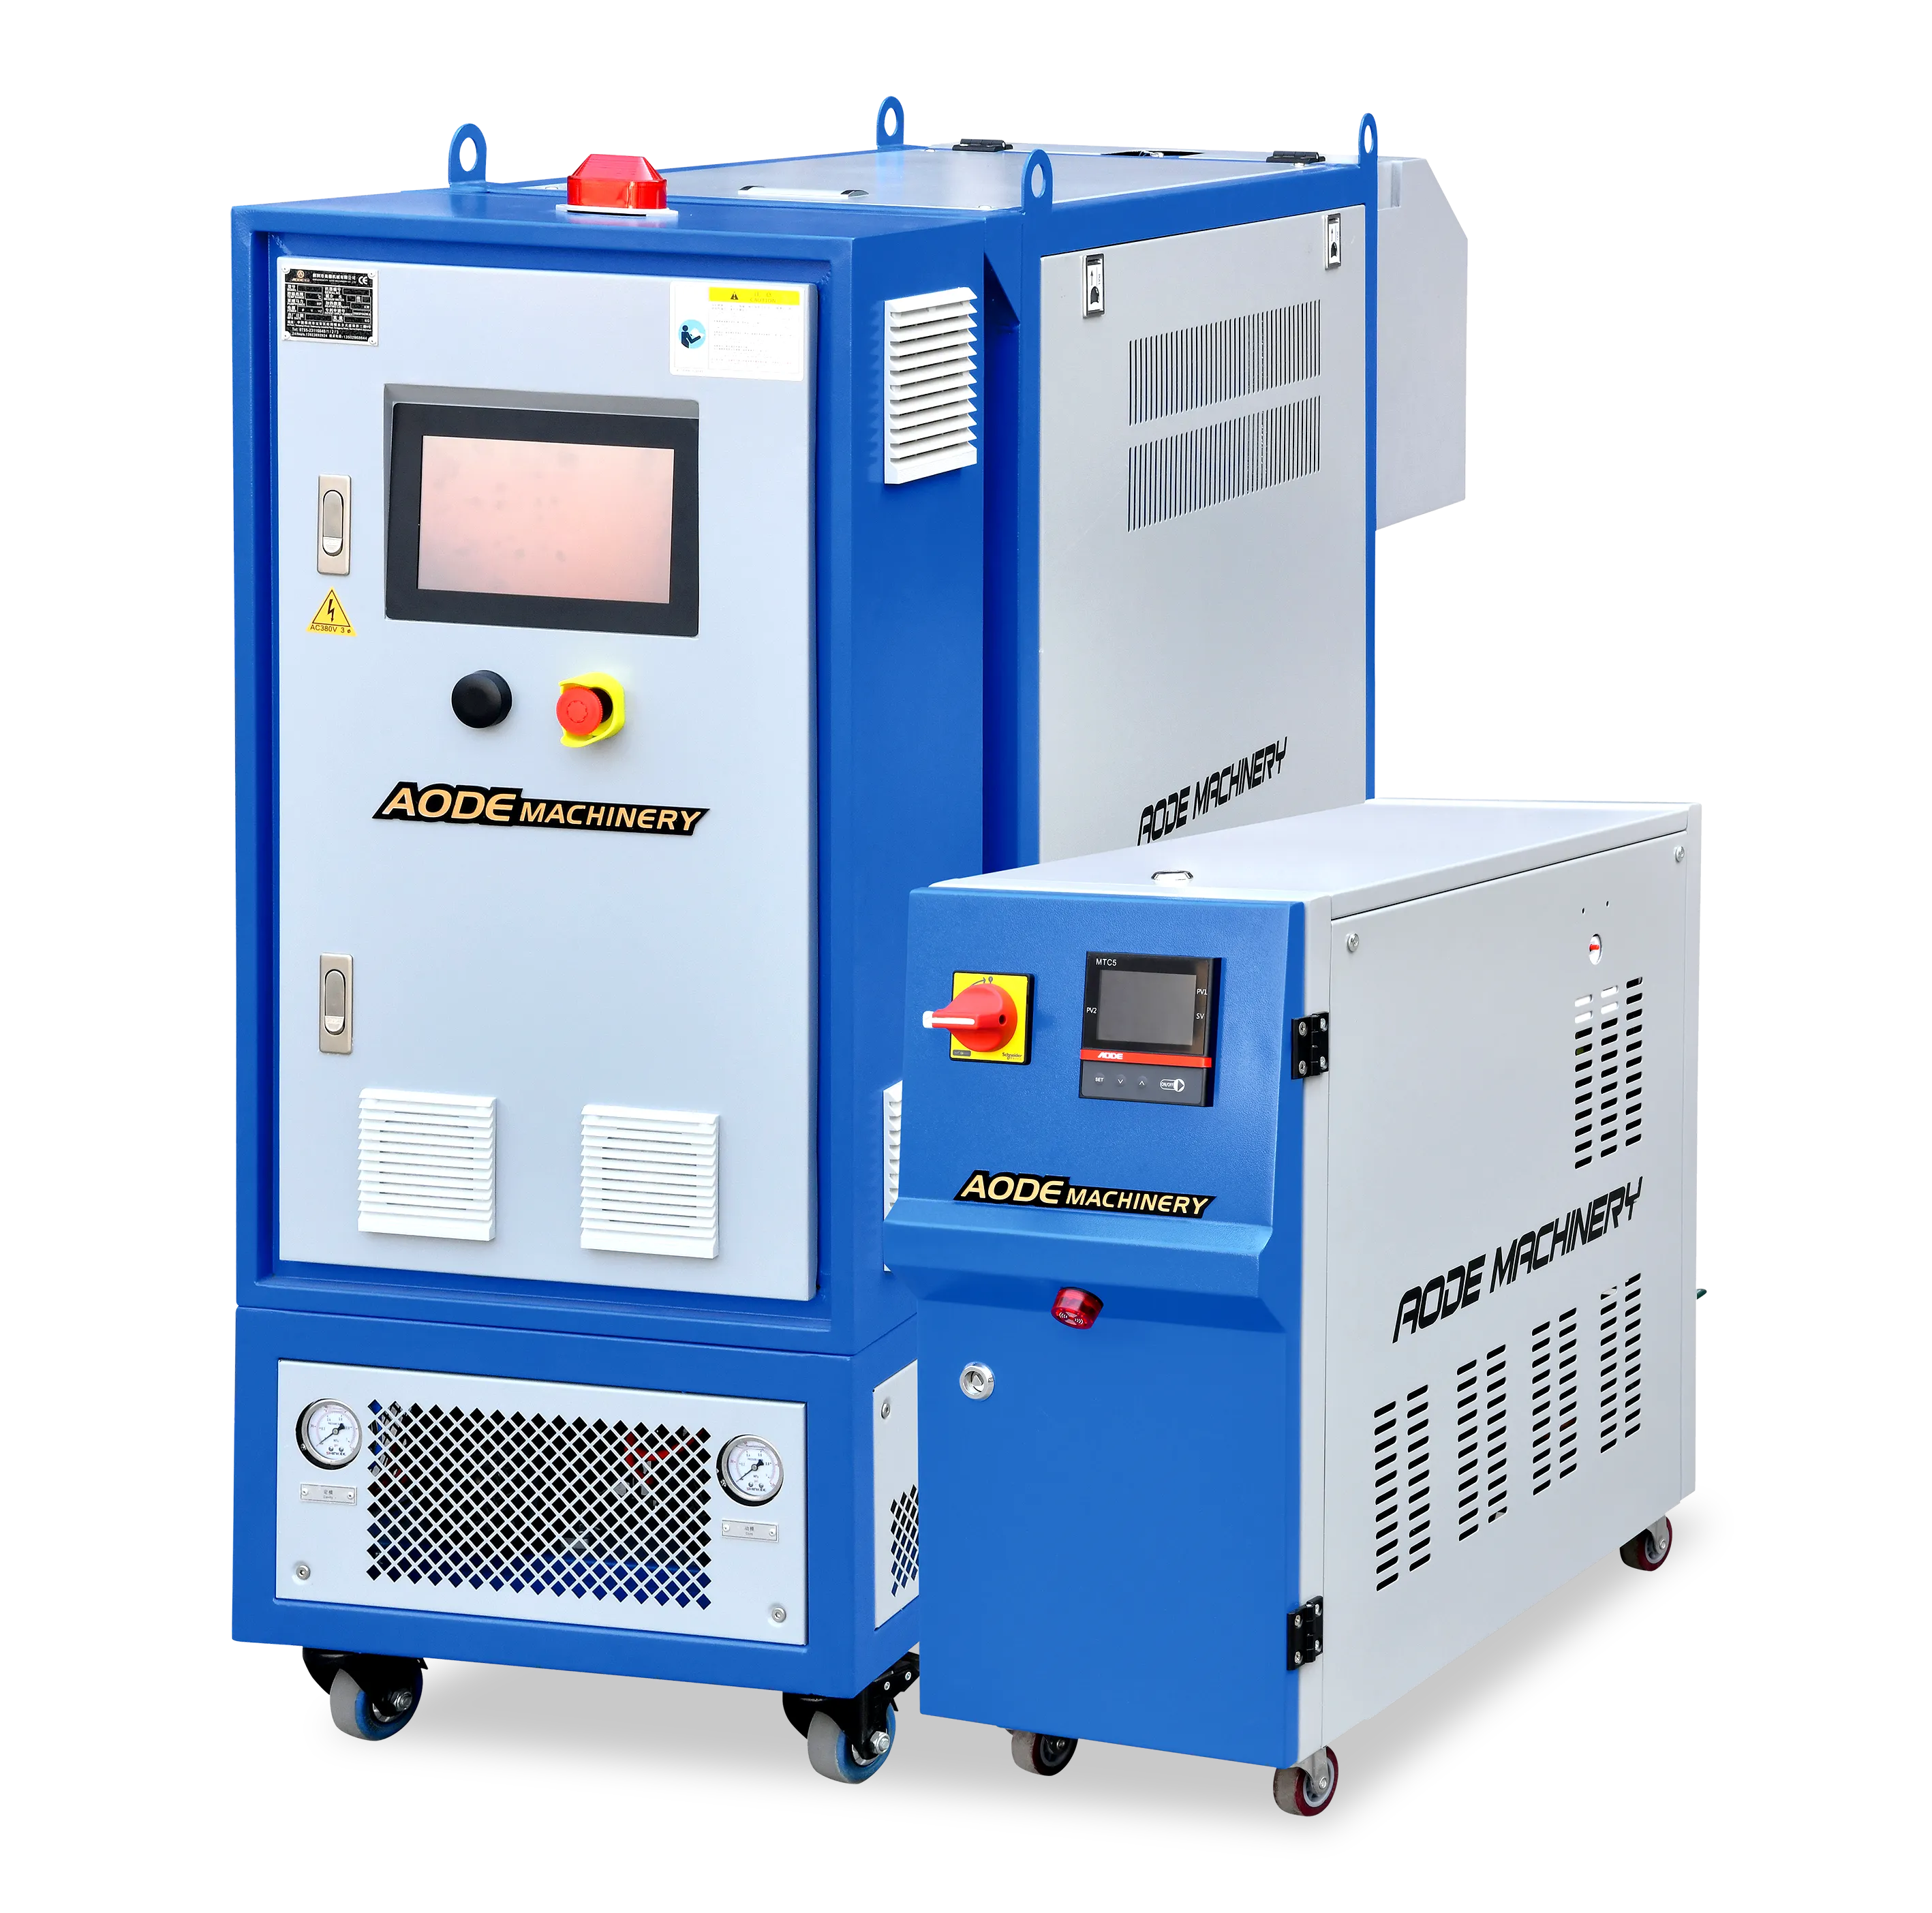
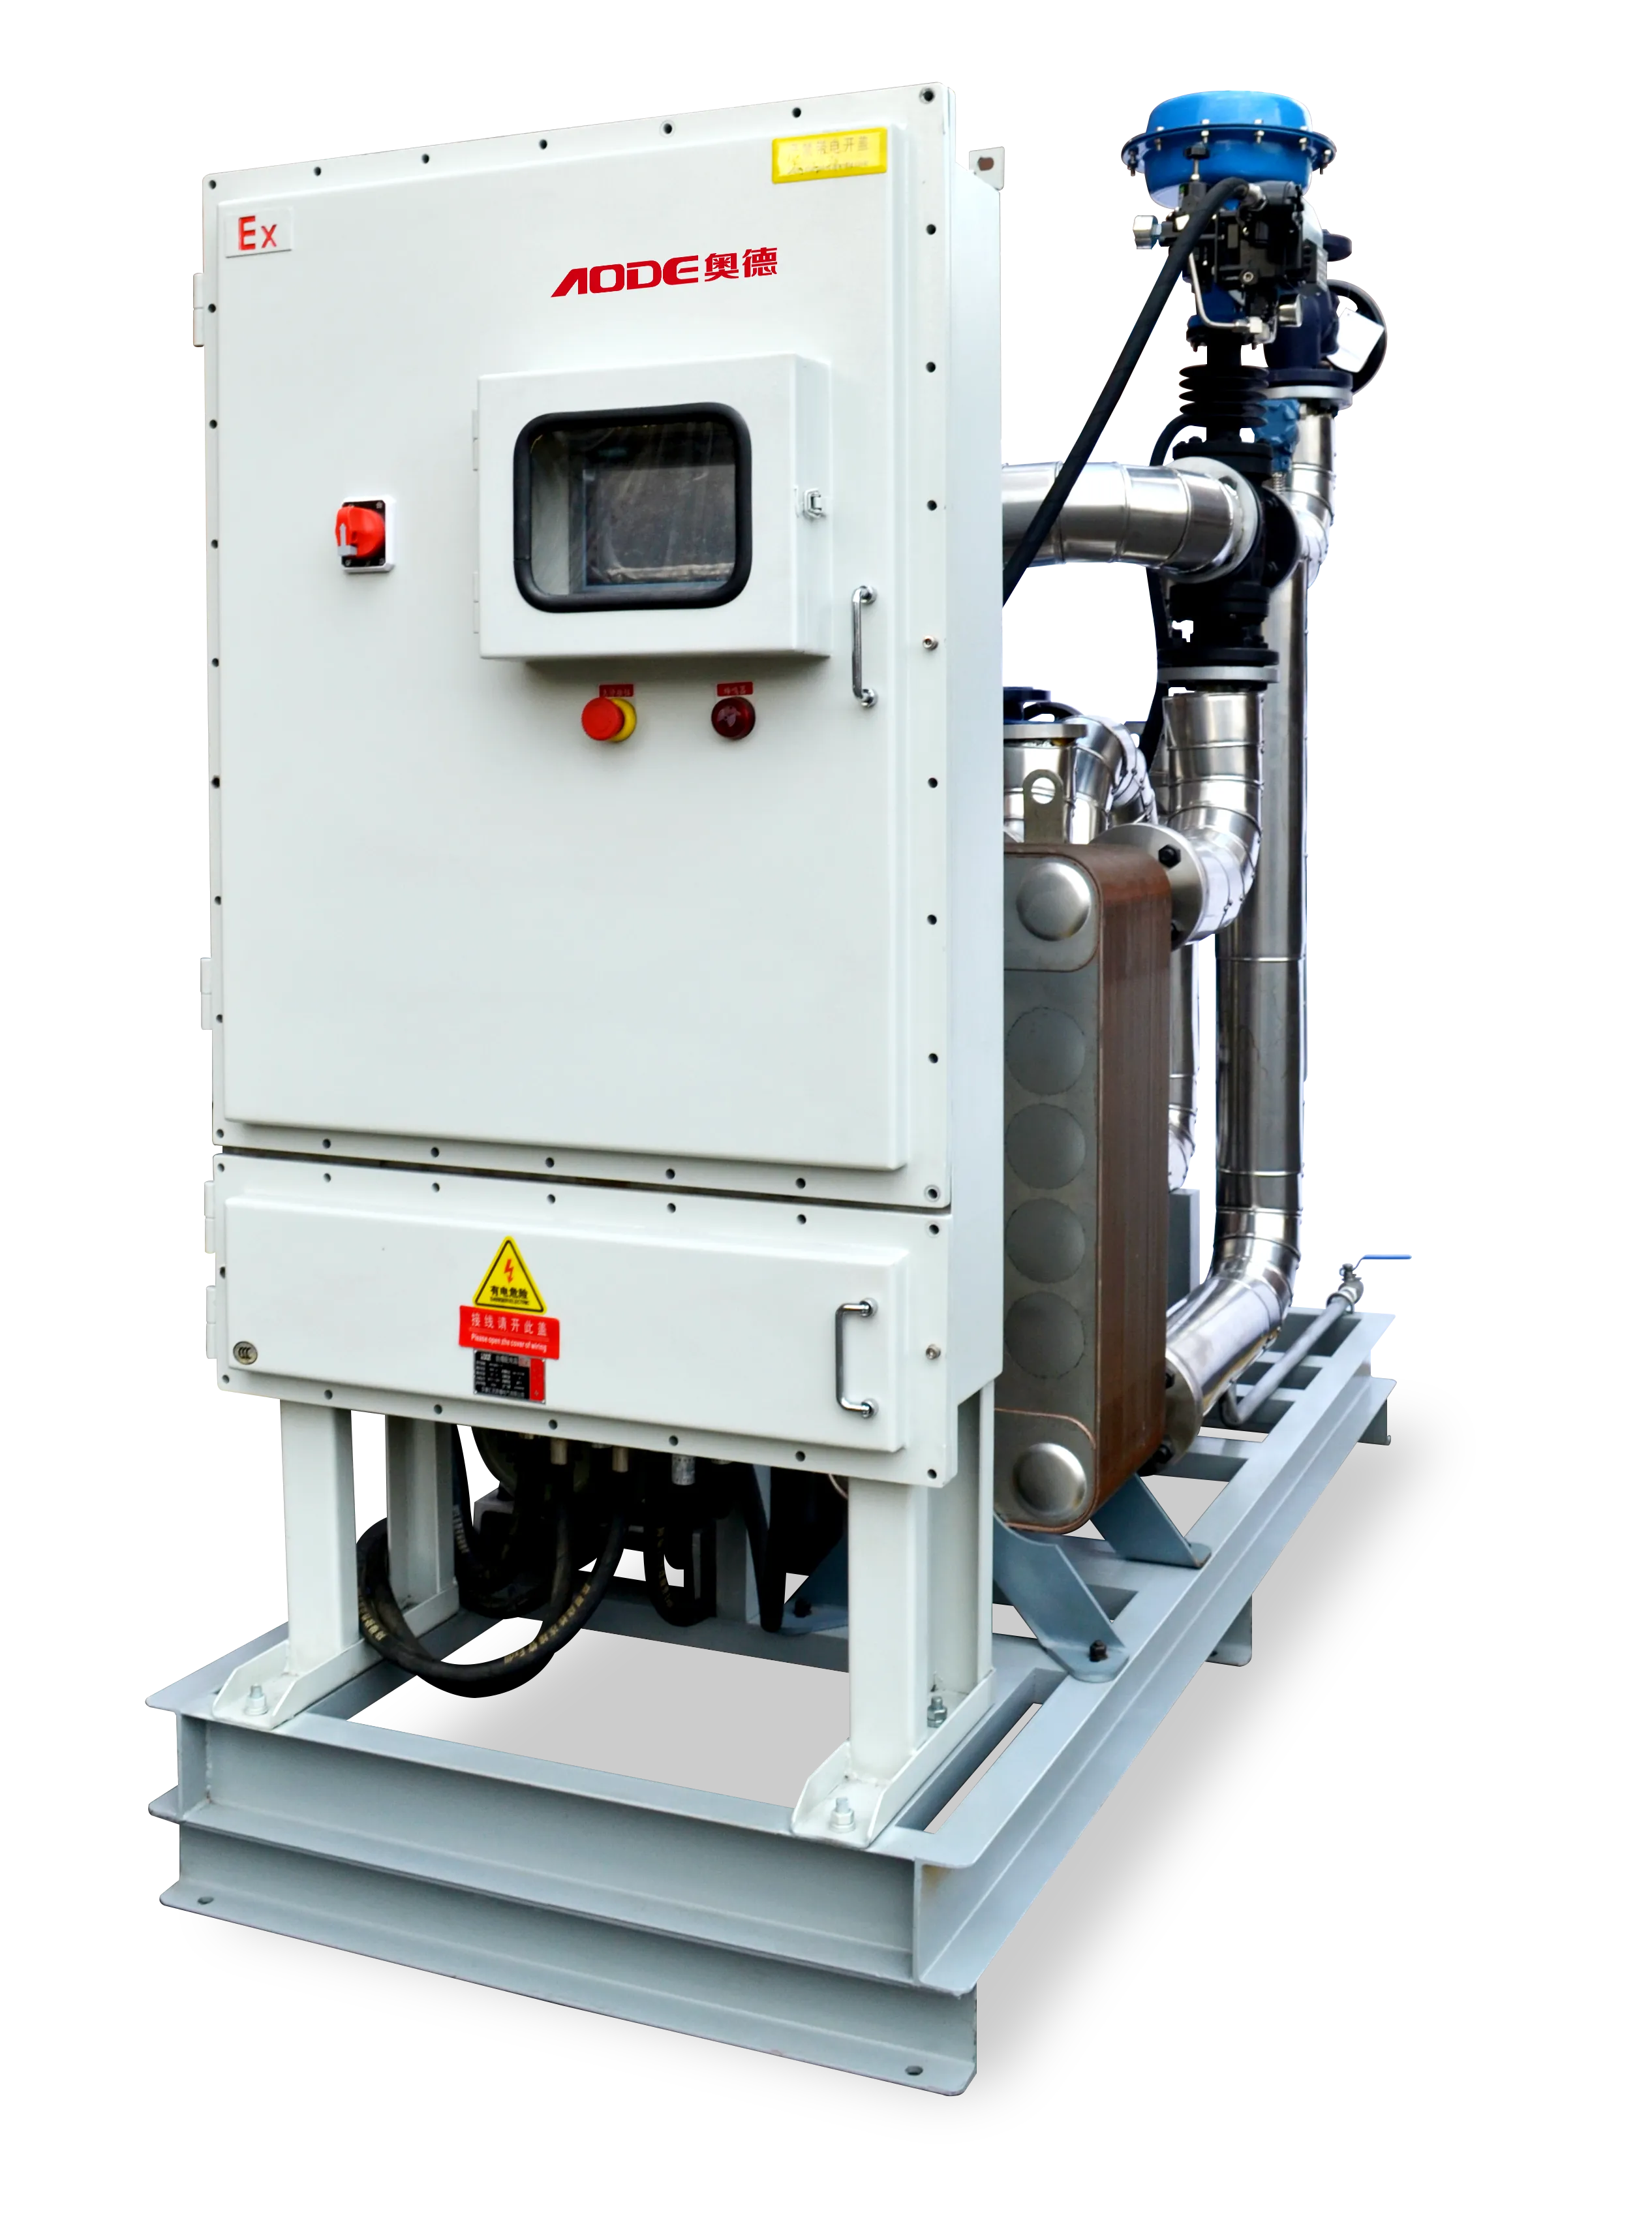
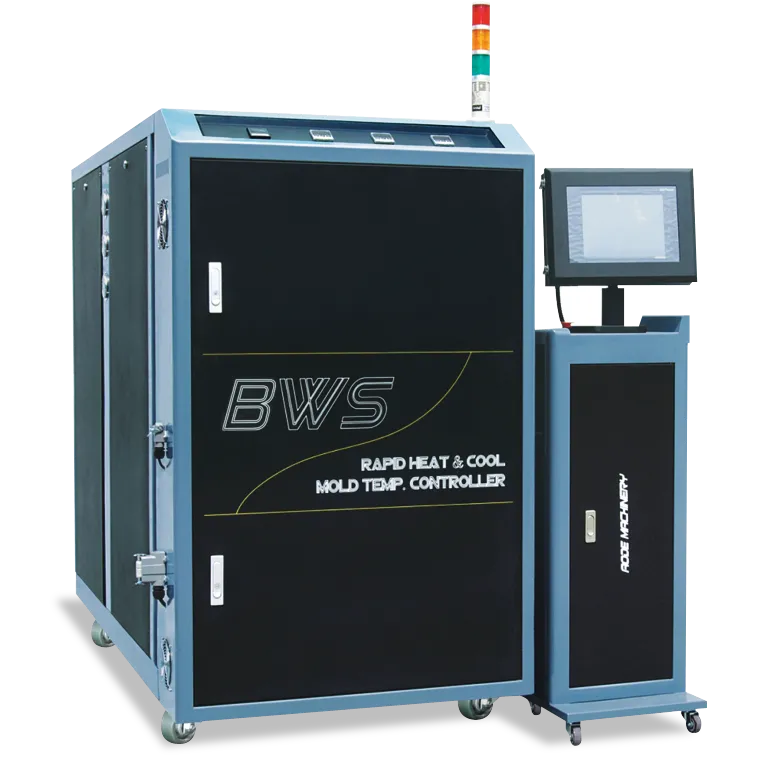
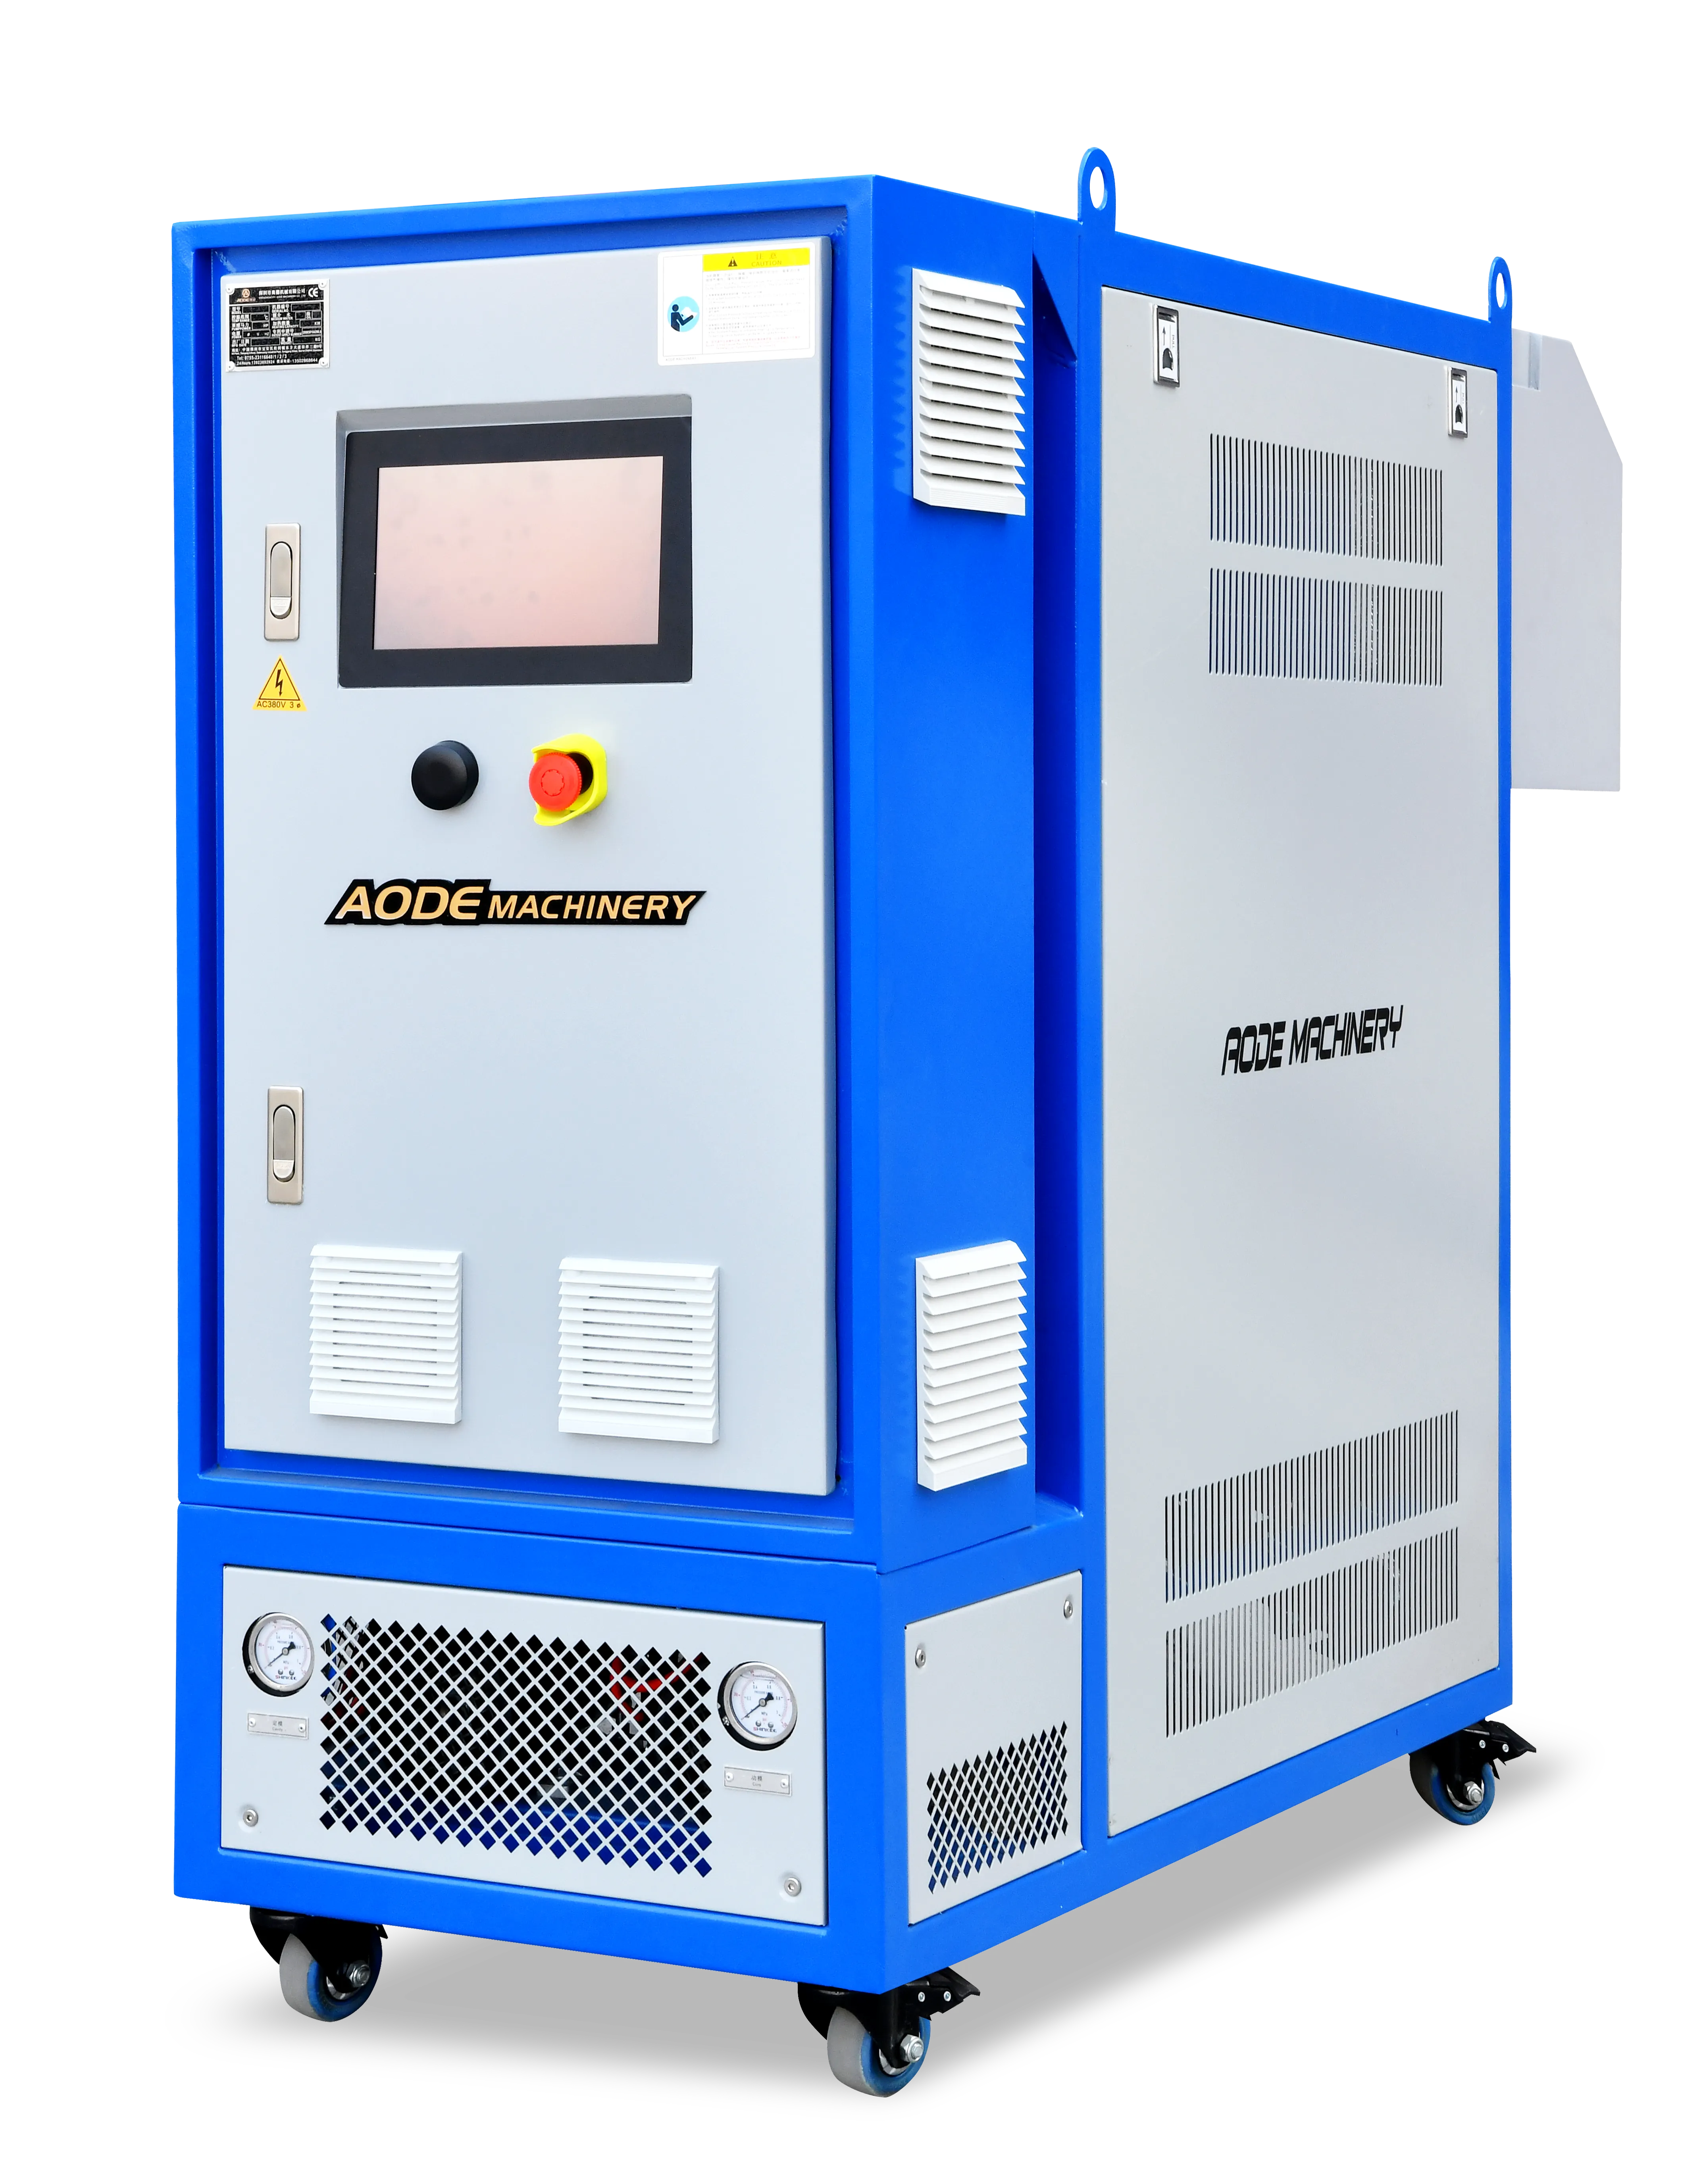
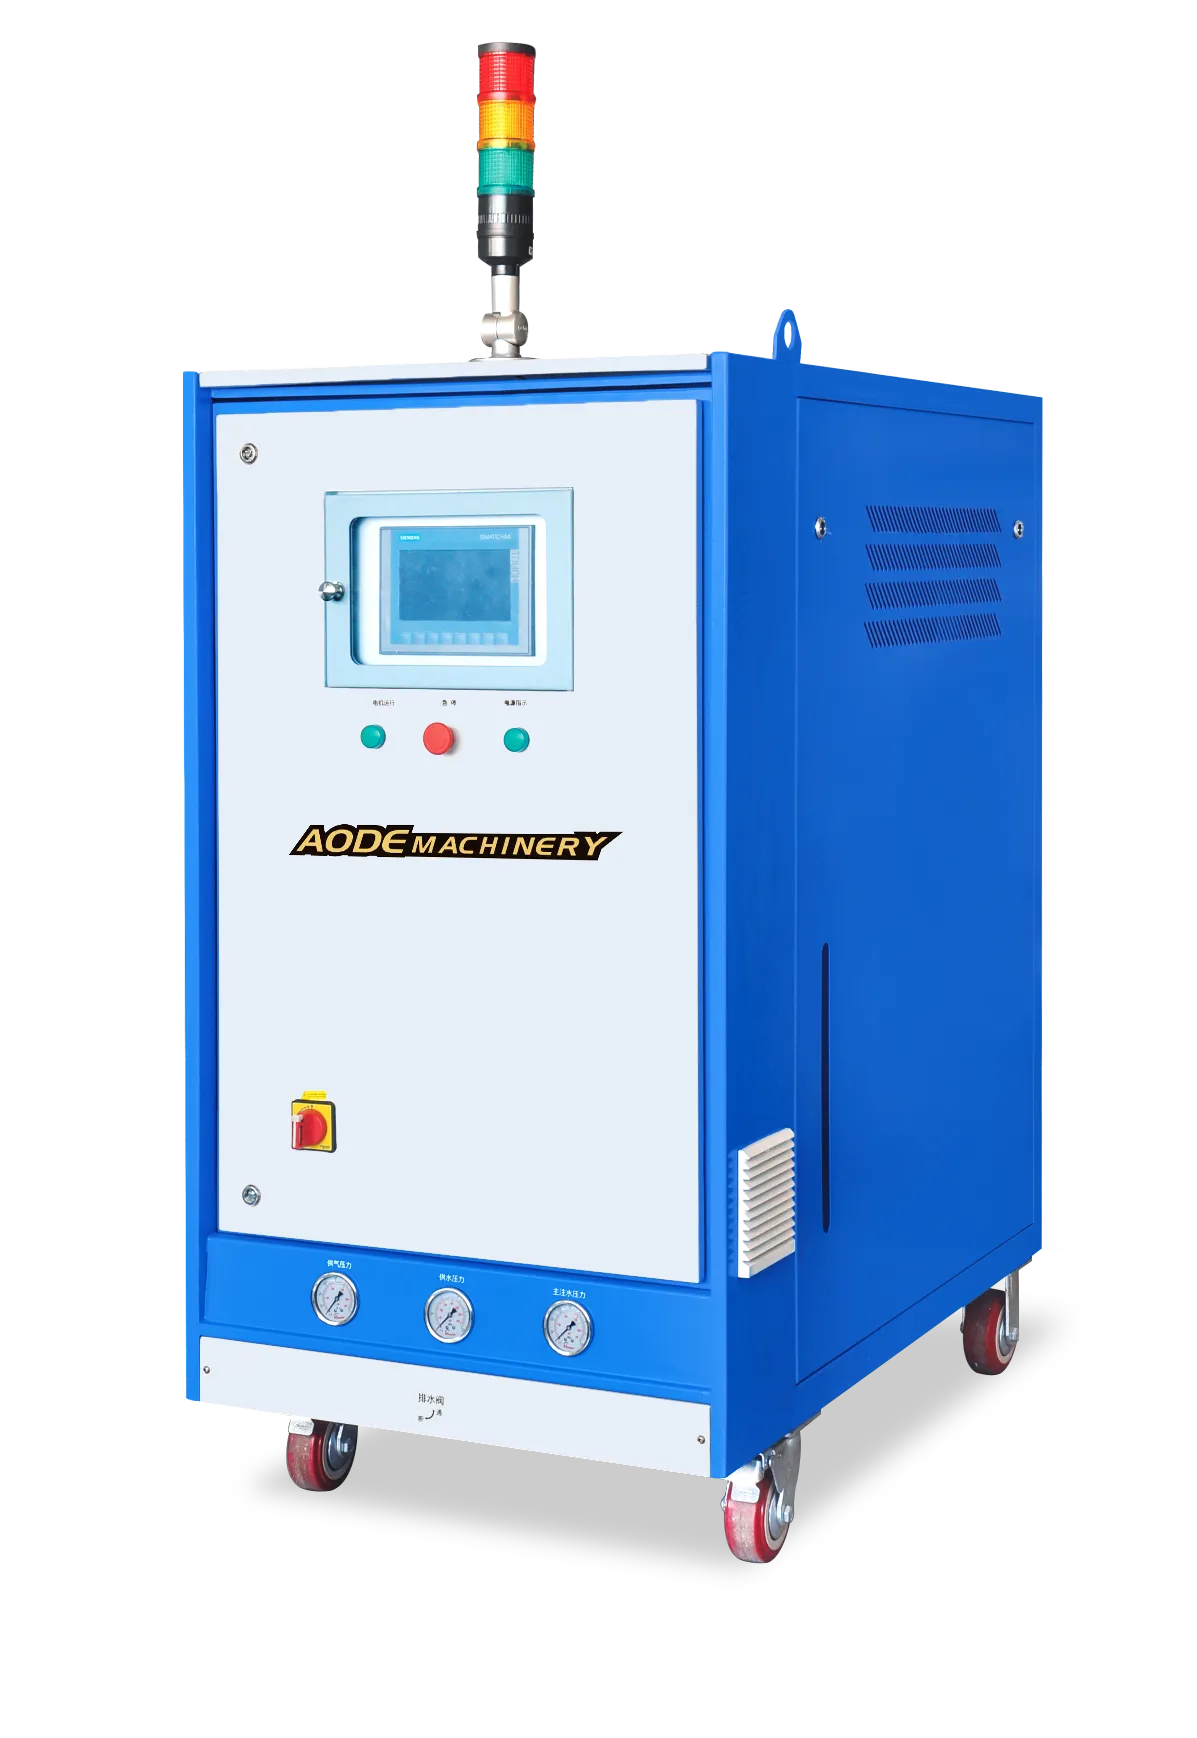
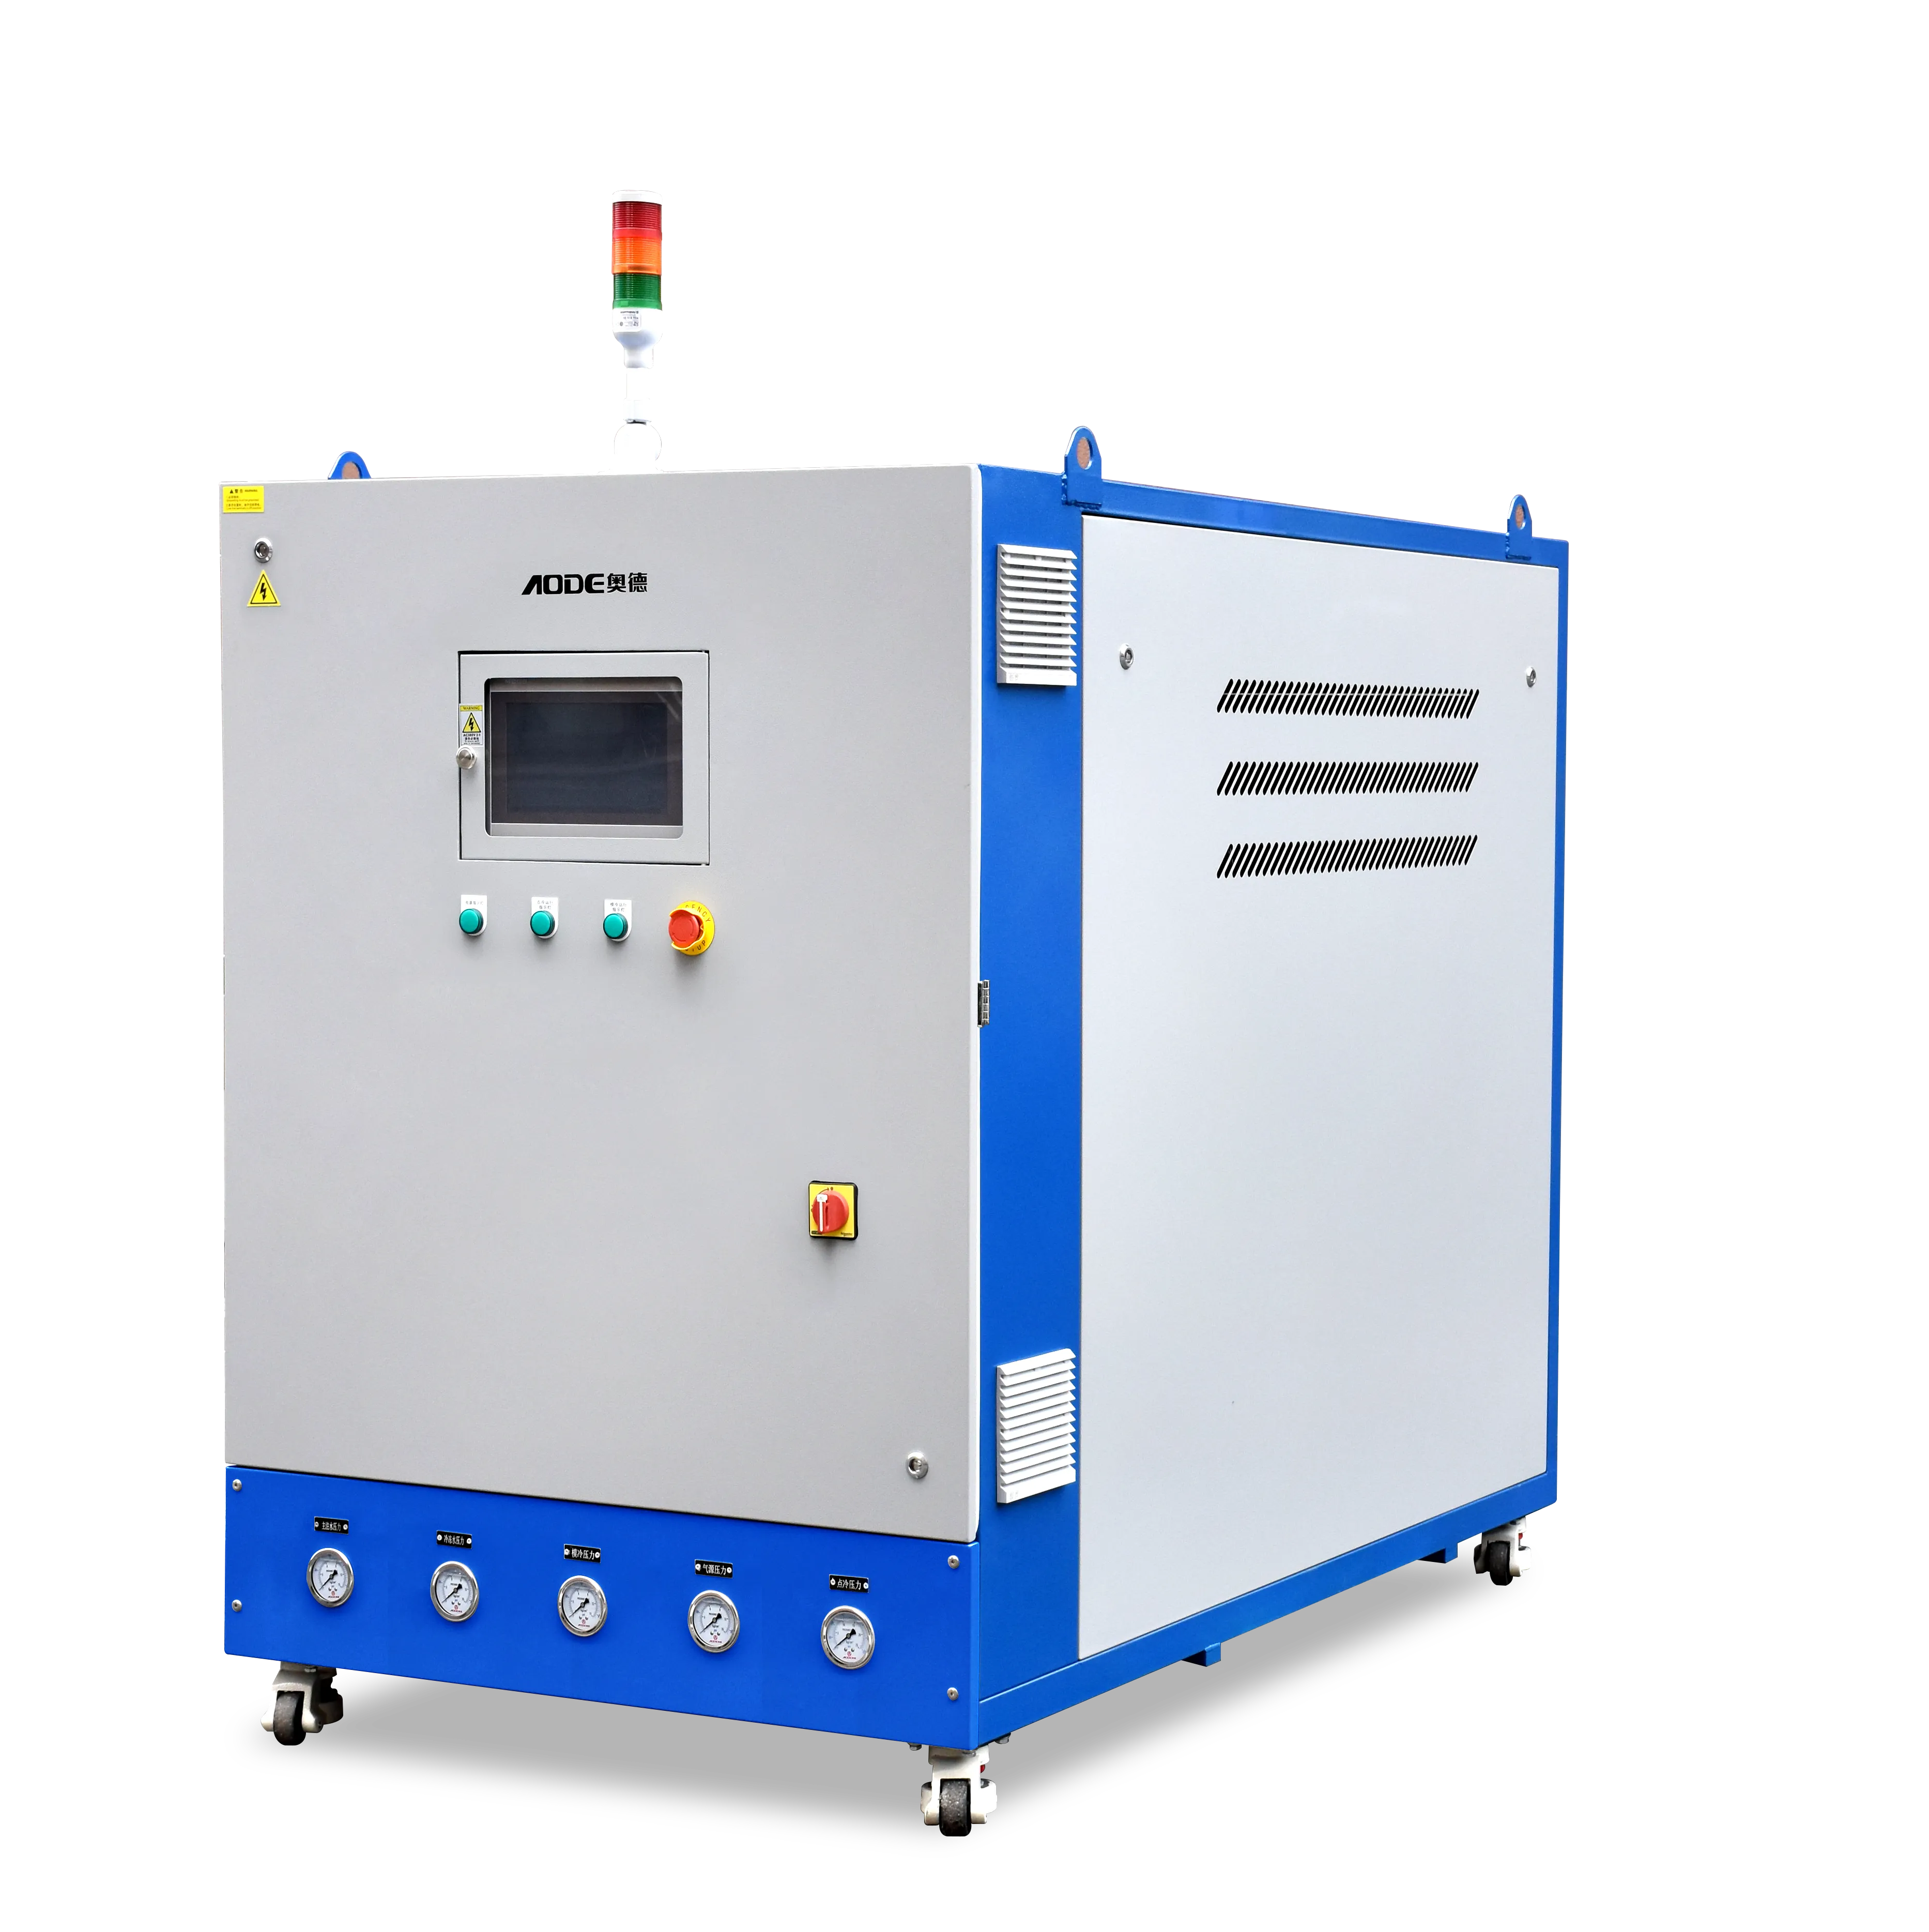
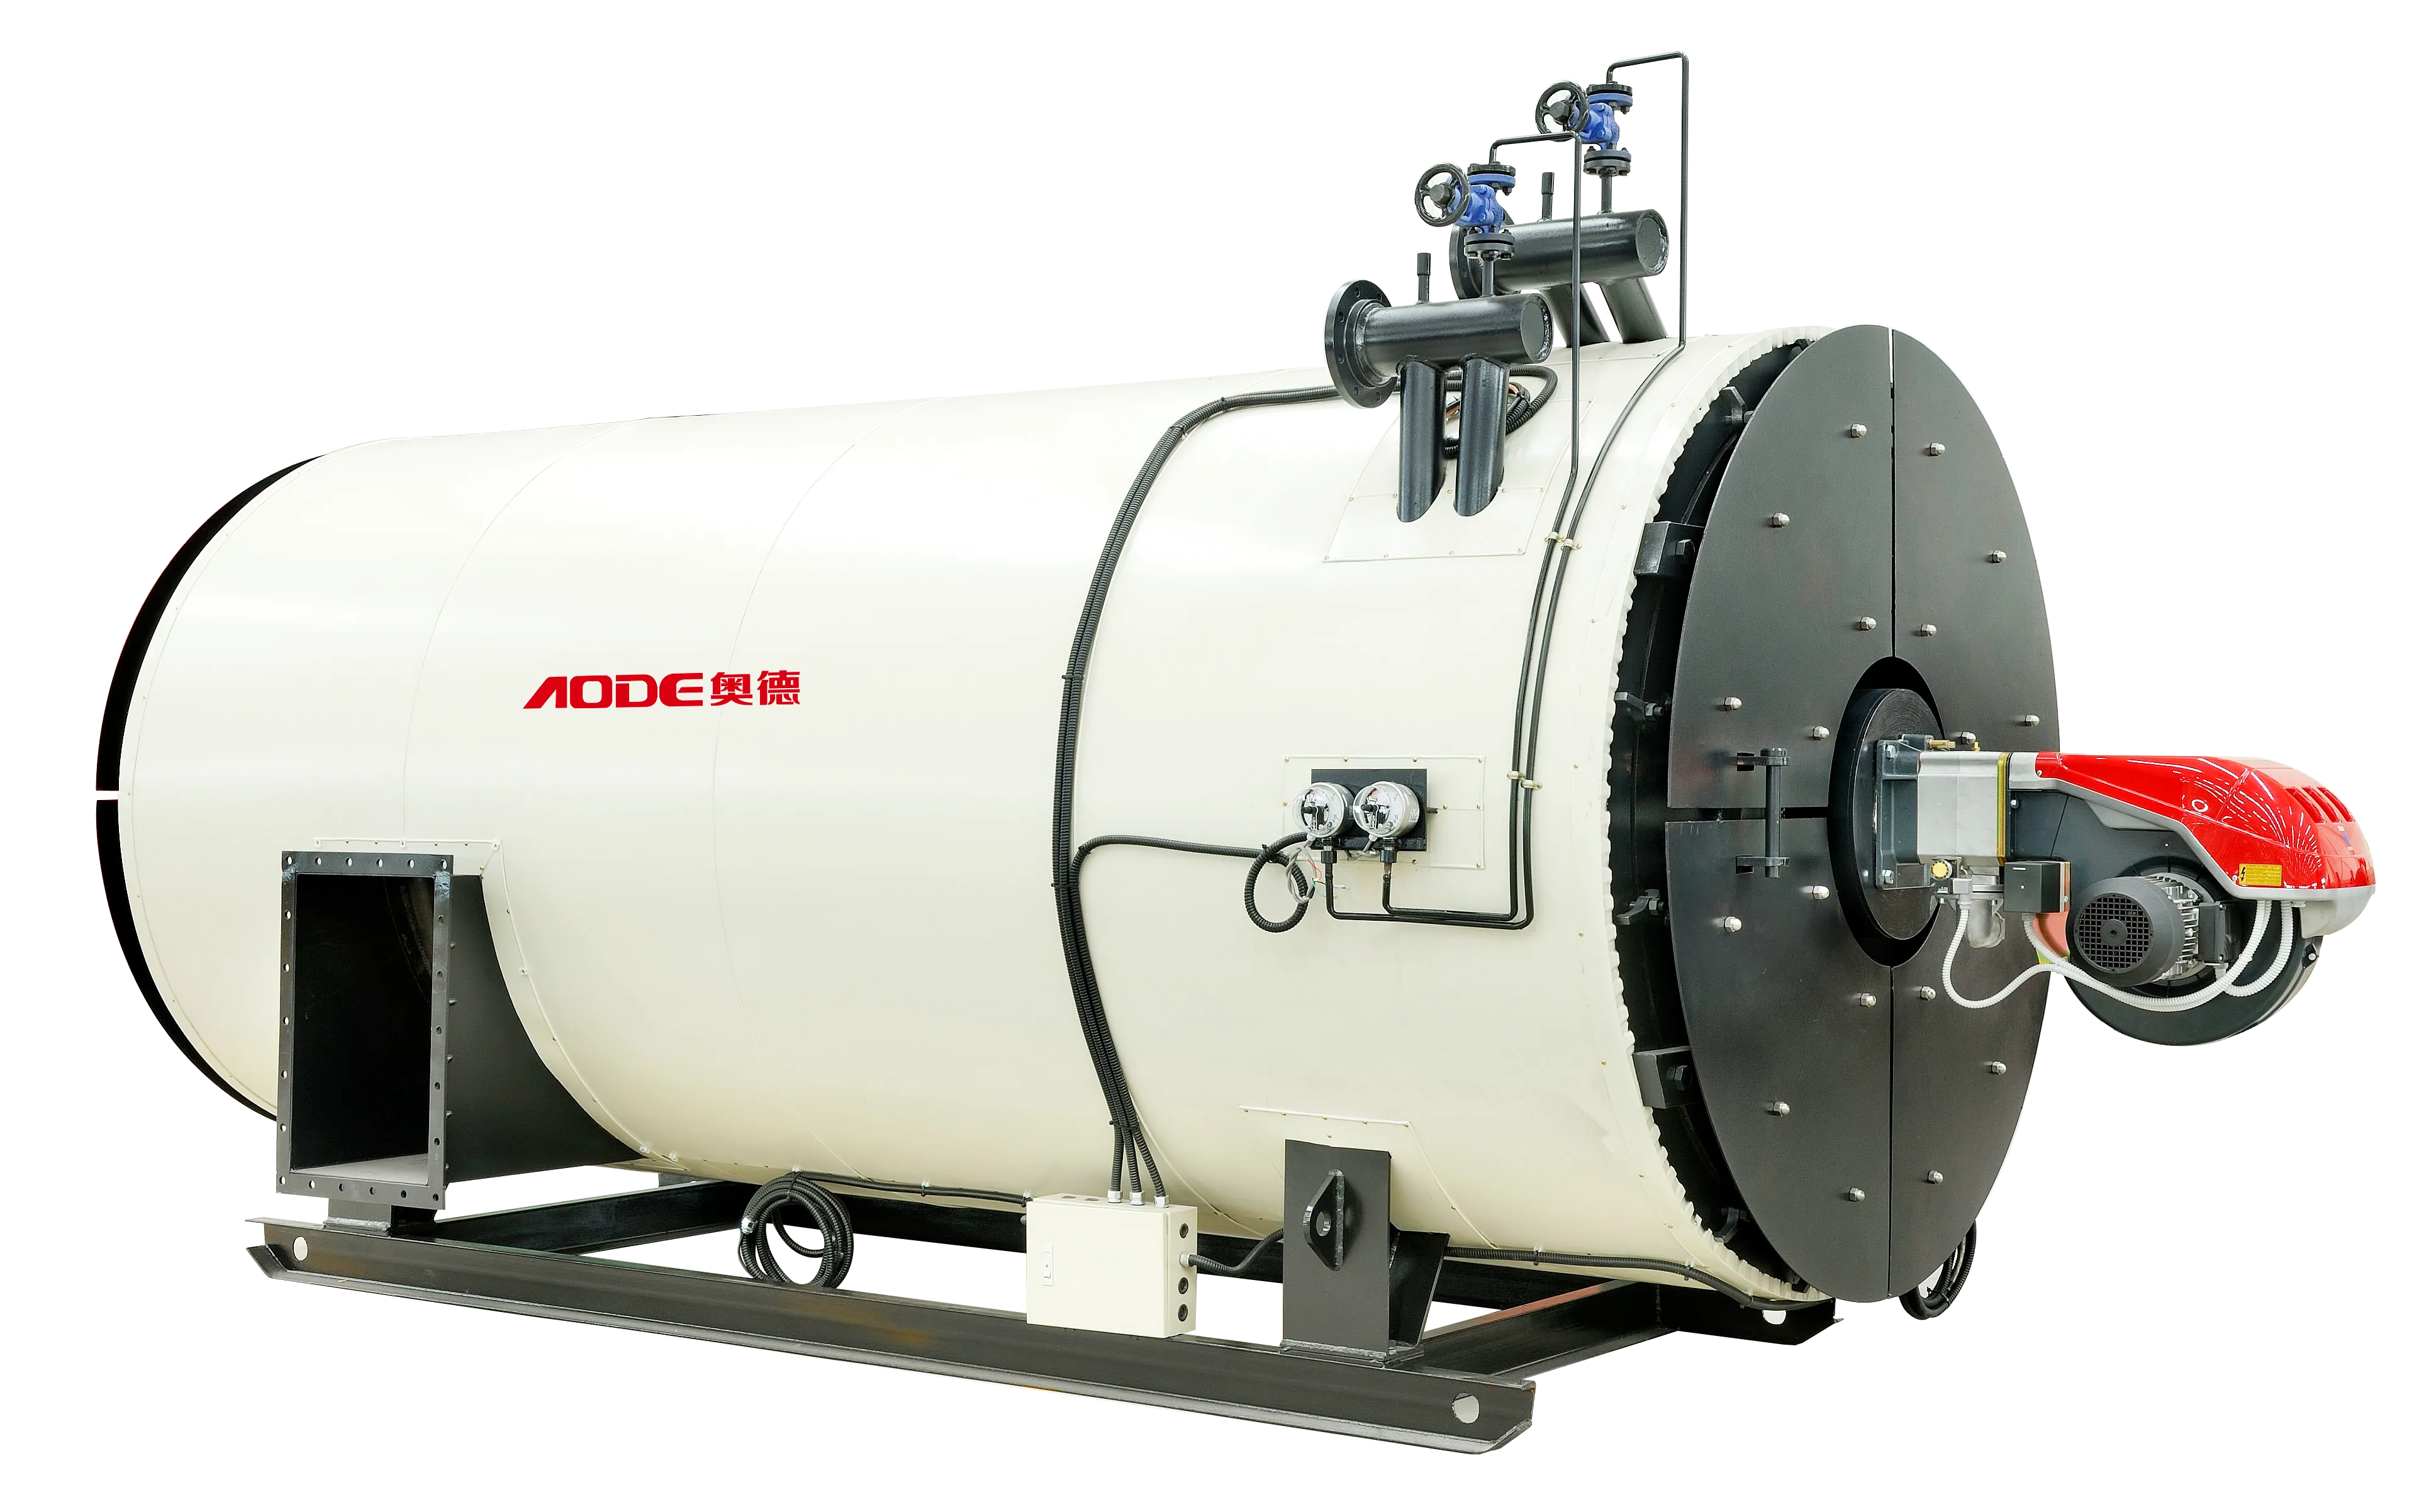
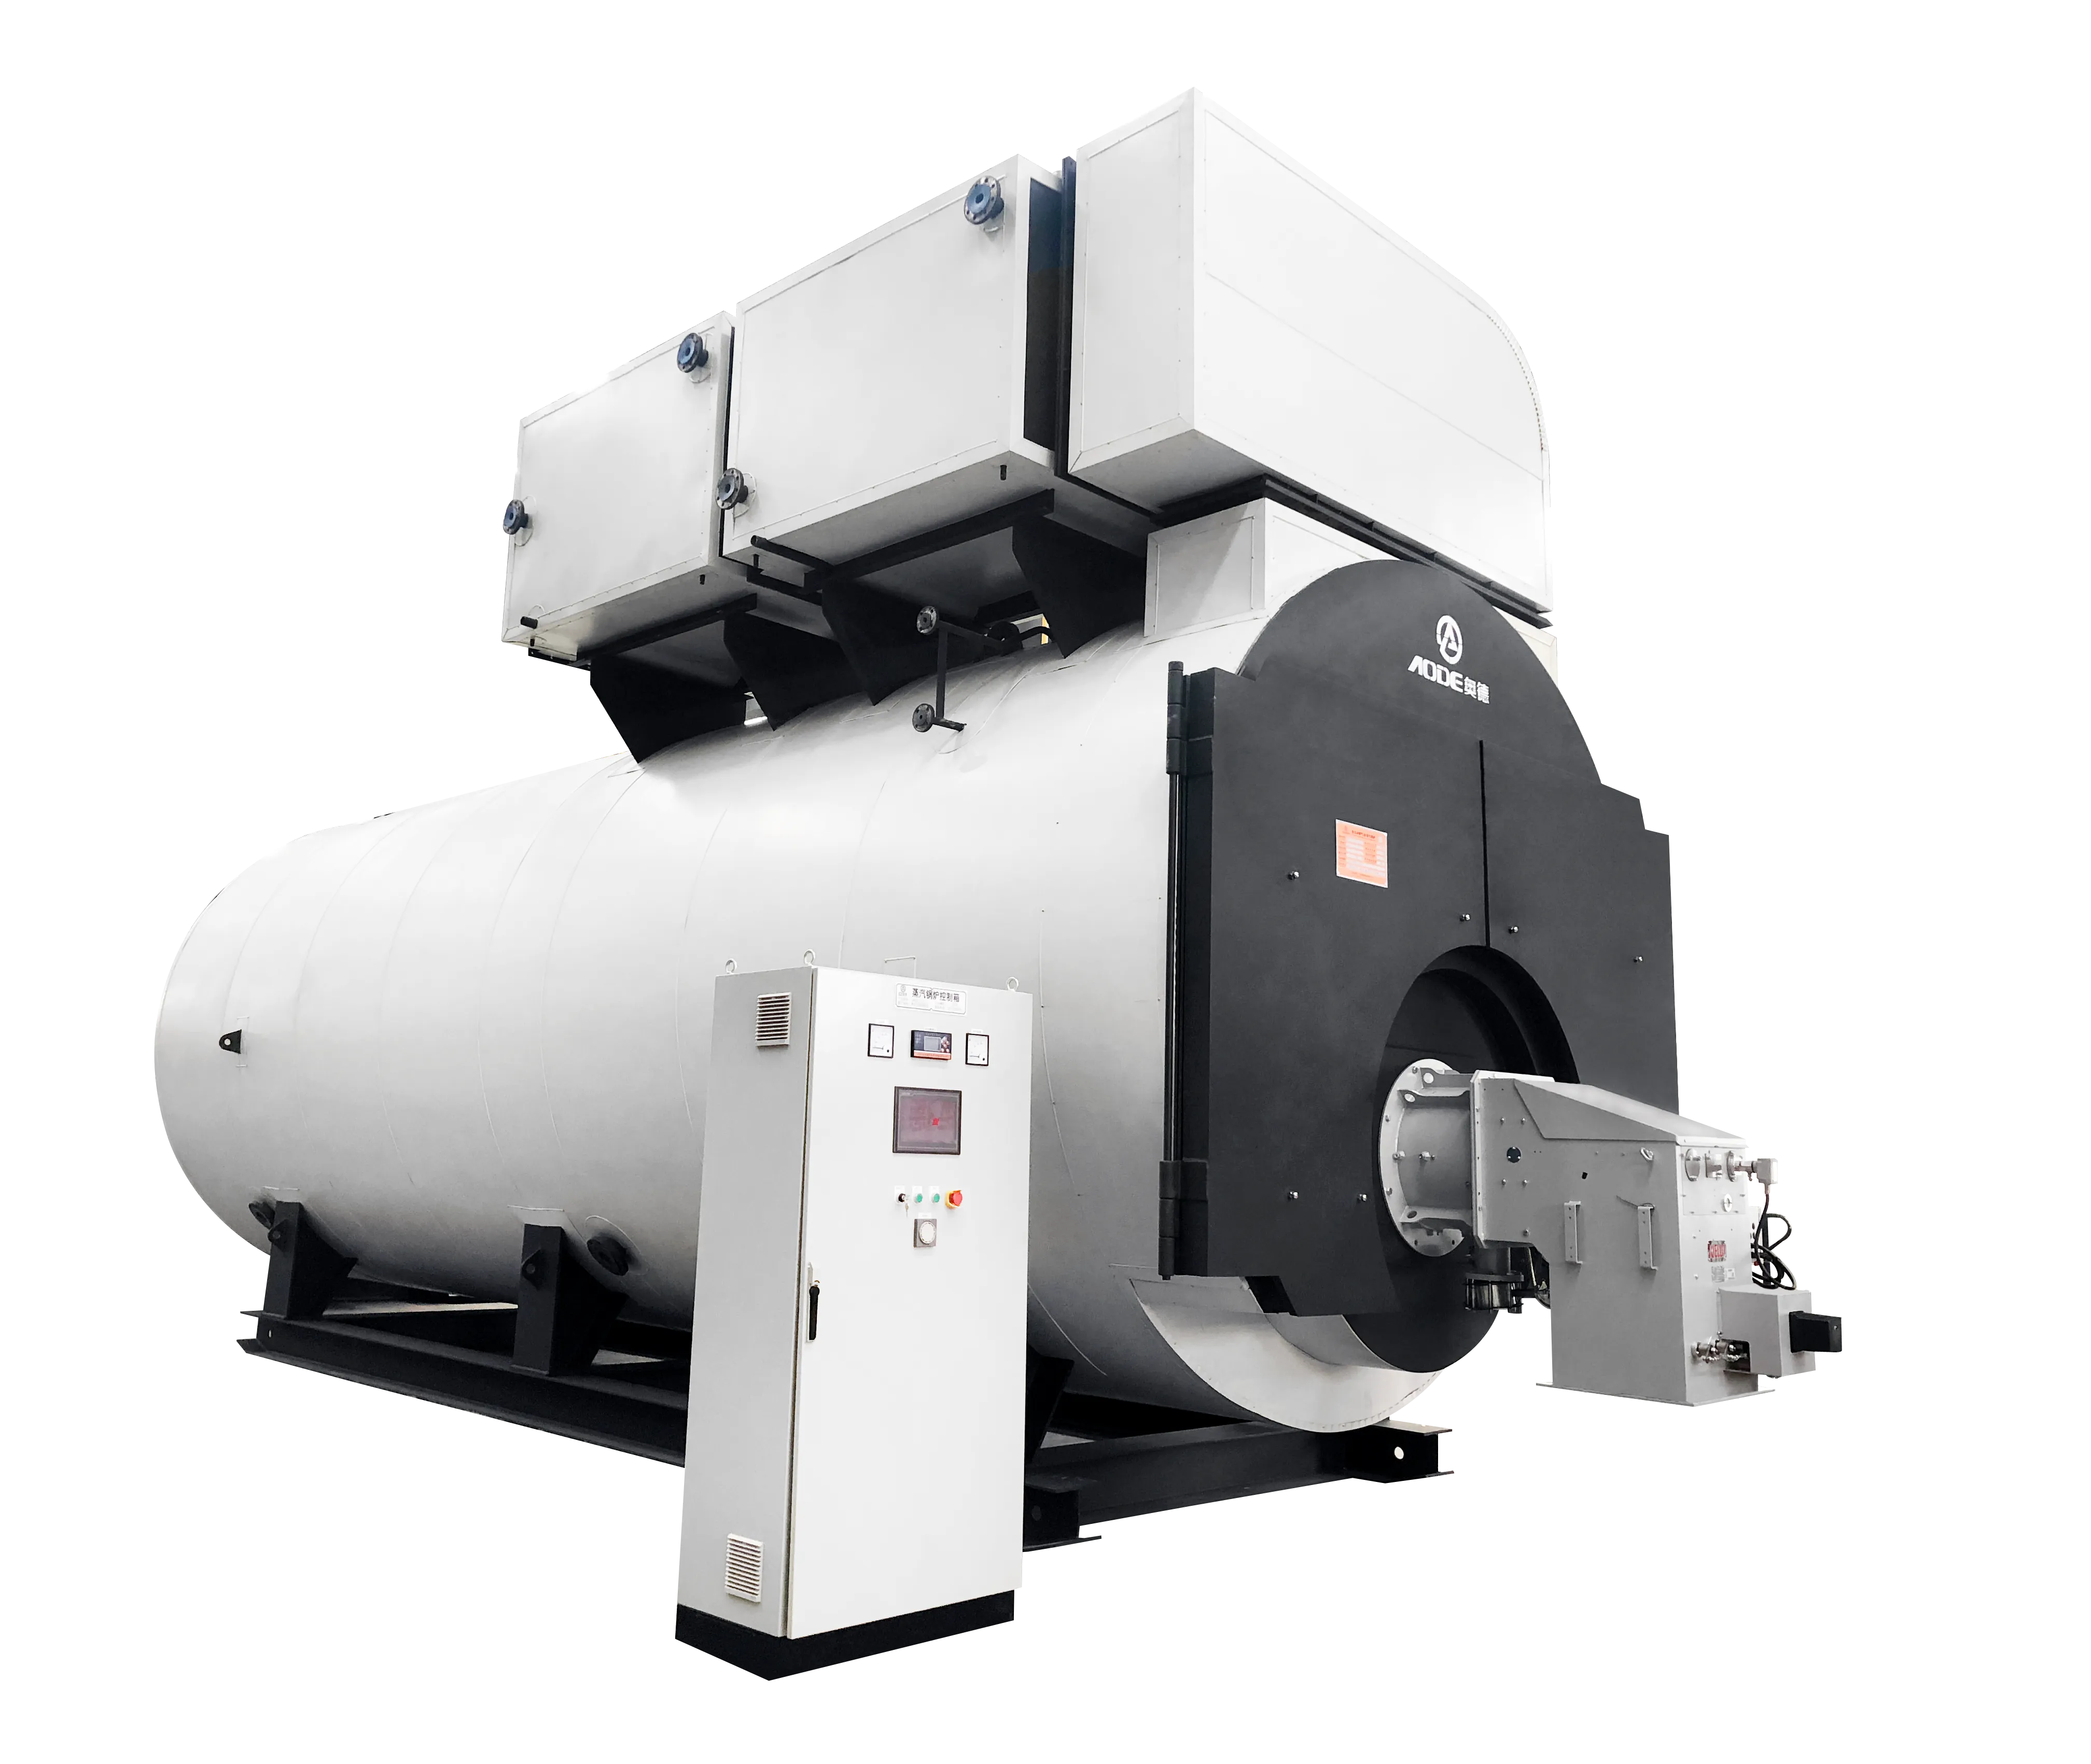
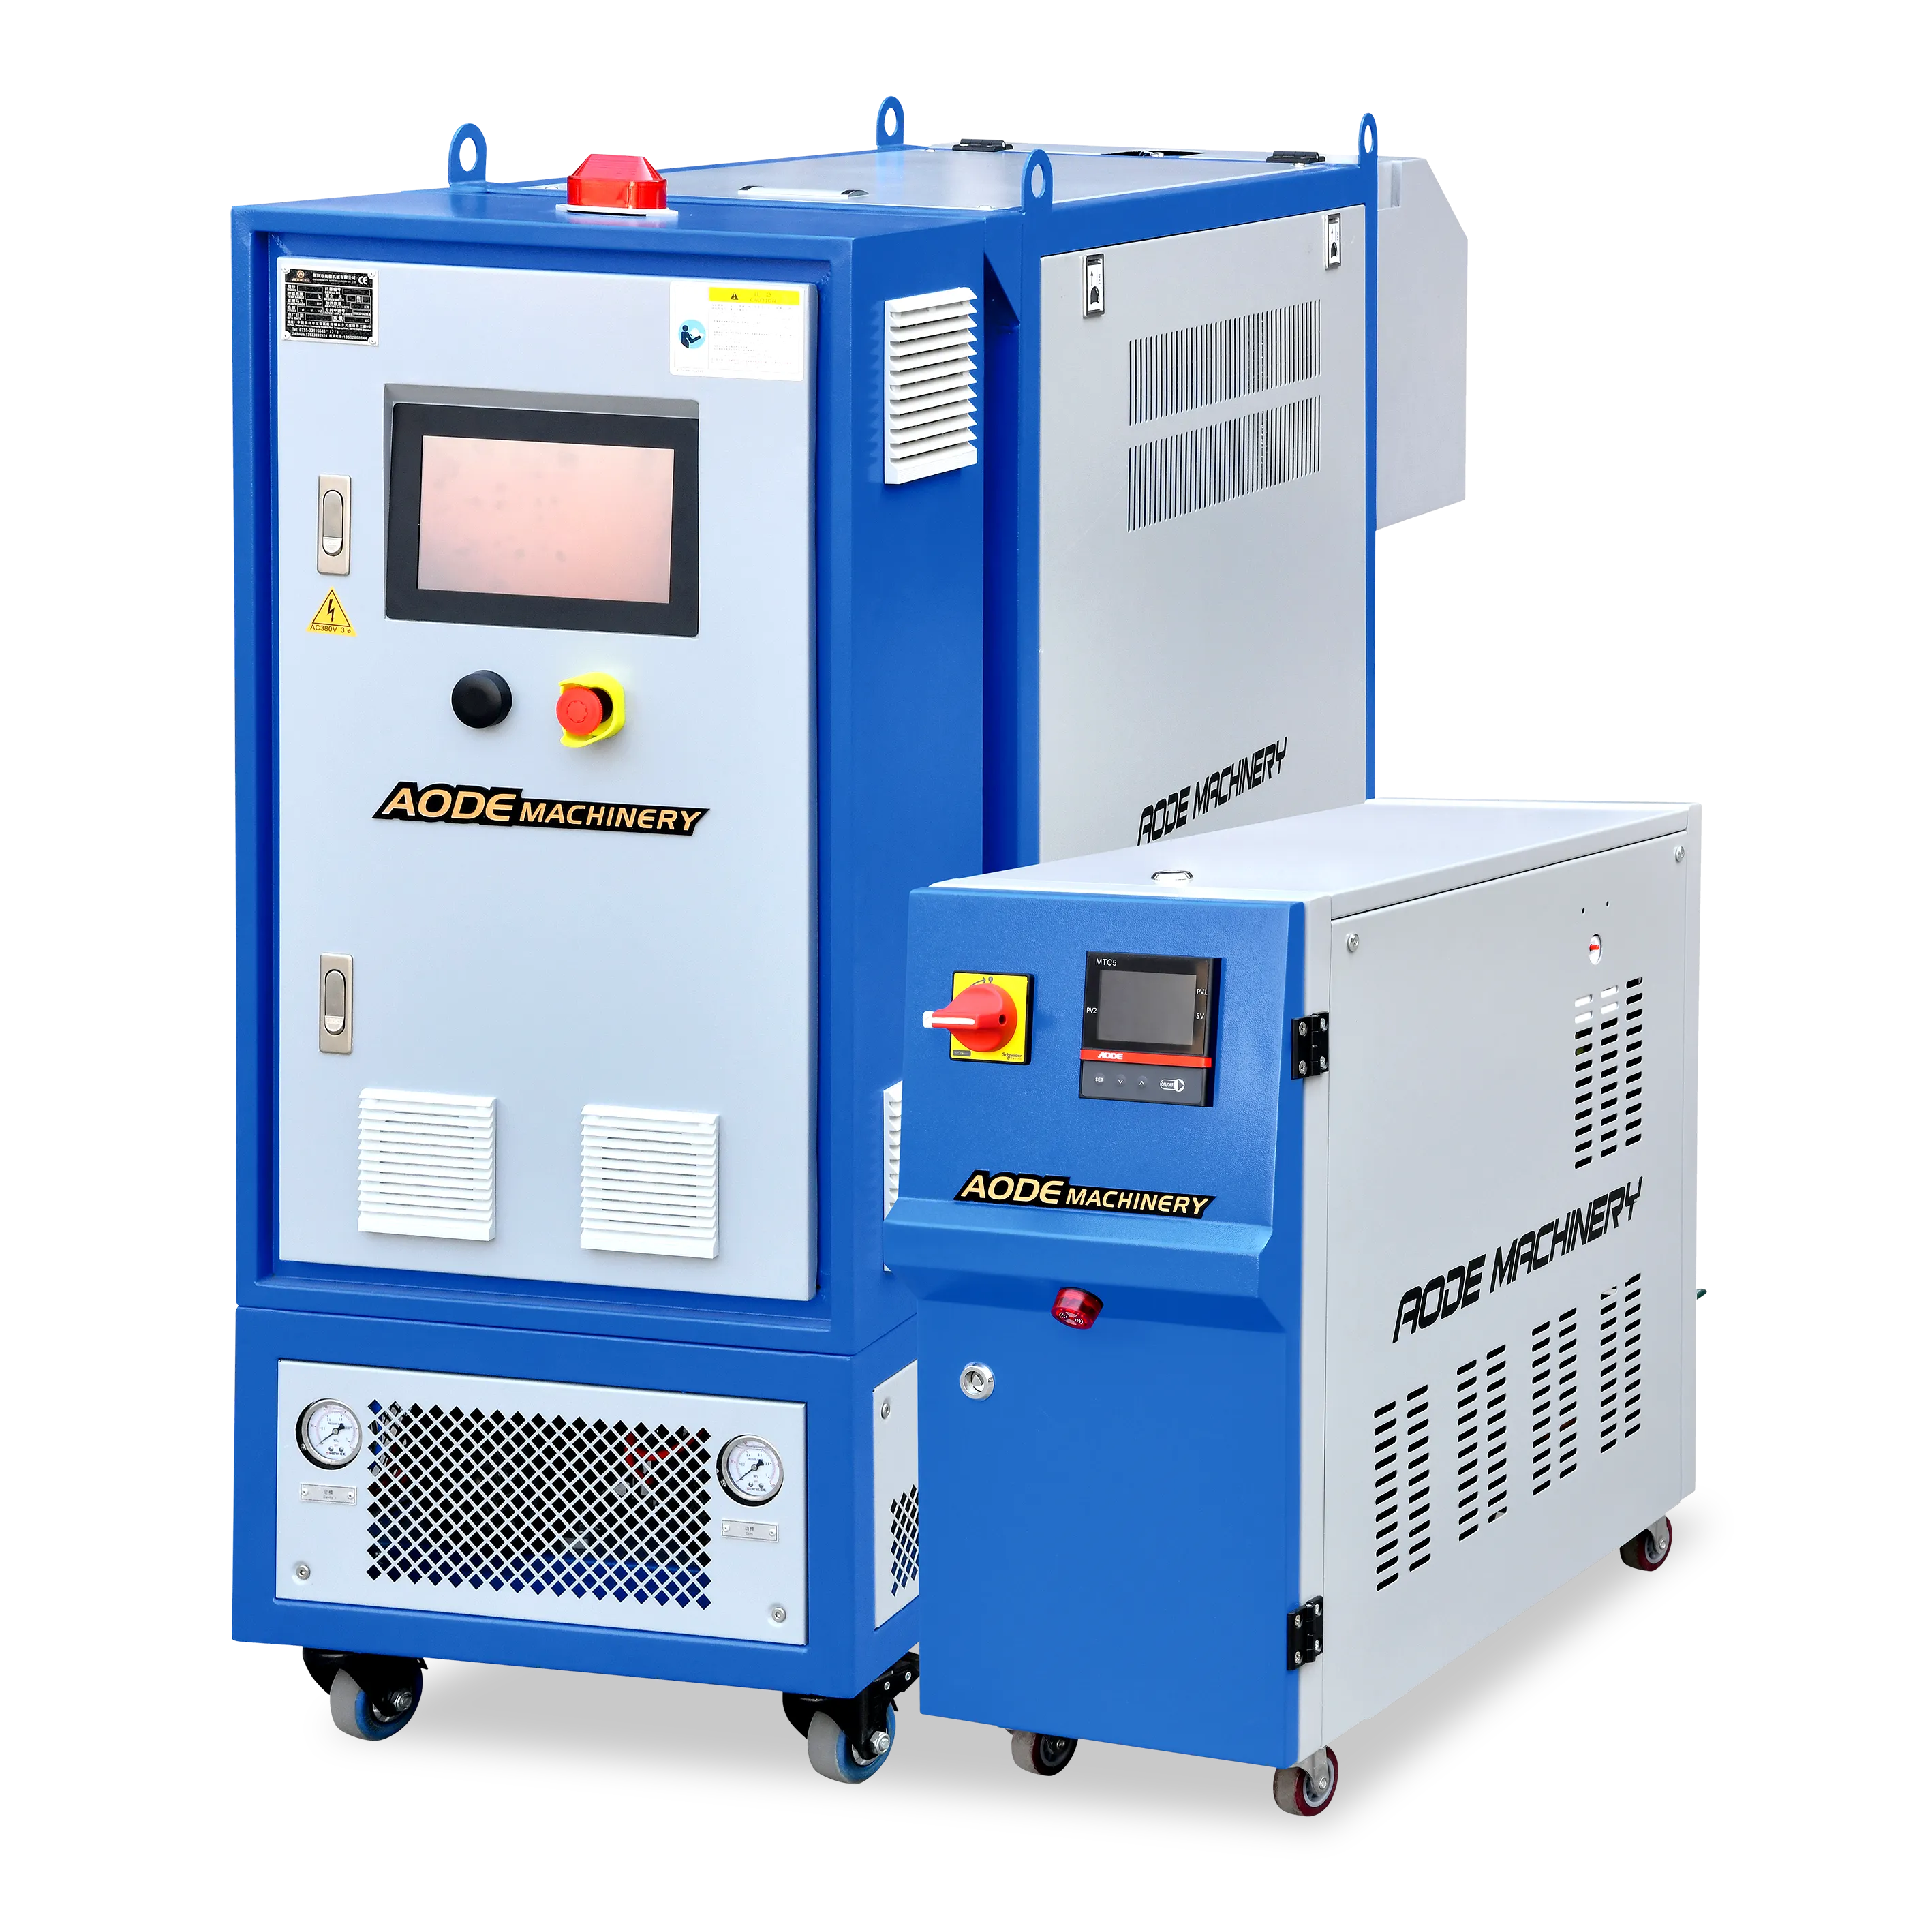
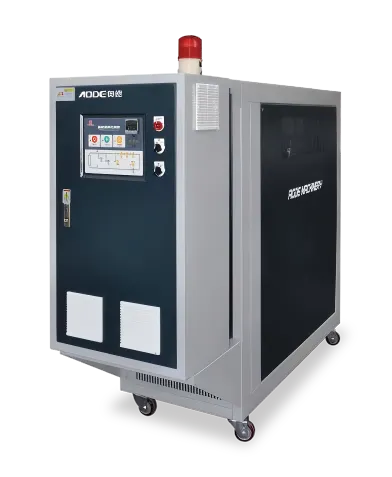
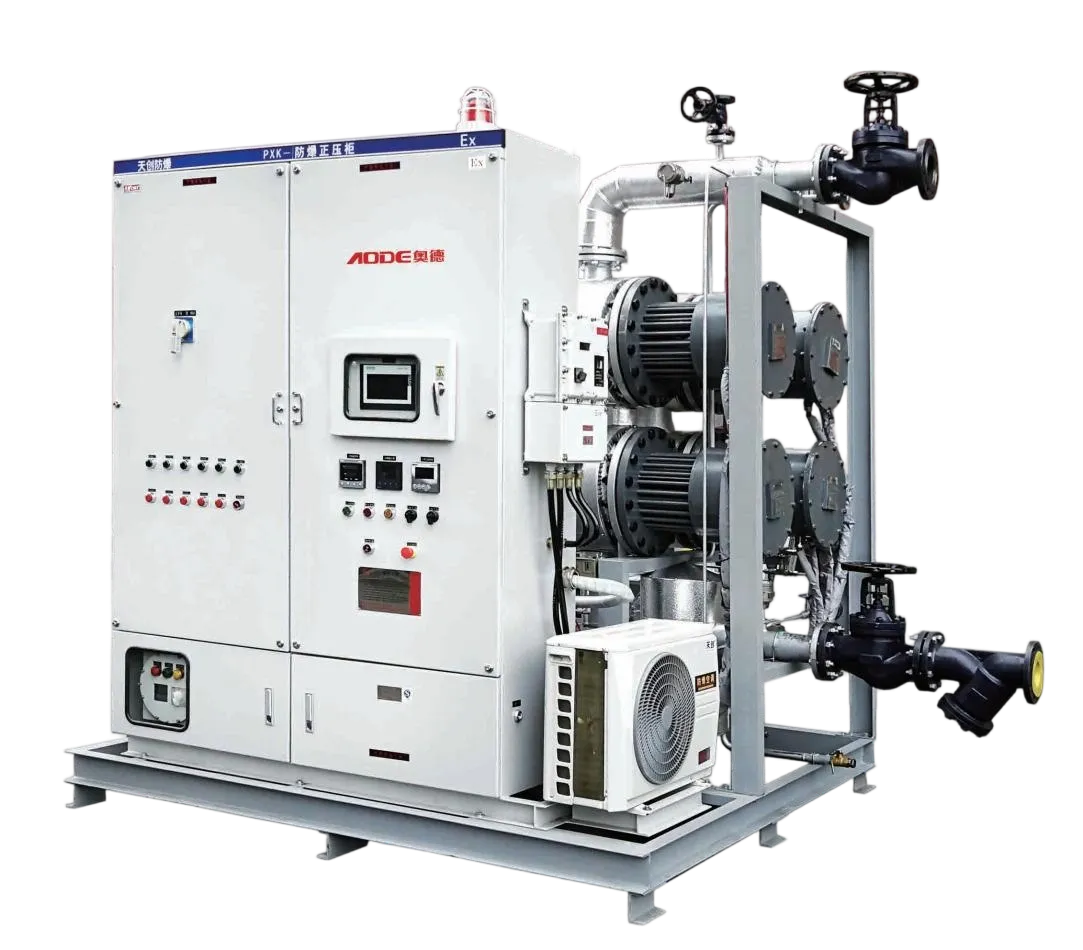
Electrically Heated Organic Heat Transfer Fluid System
Temp Control Range: +45℃  +400℃
Features
Explosion-proof device、Blow-up oil return function (optional)
RS485 communication function for automation management
Isolated electrical control box to prolong the use of electrical appliances
Pipeline using organic heat carrier furnace special pipeline
Perfect safety protection, fault display, maintenance, repair and maintenance of no need for professionals
Request a Quote
Thermal Fluid Heating System Specifications
| ITEM | UNIT | YWDR0.12- 0.5/300/280 | YWDR0.24- 0.5/300/280 | YWDR0.3- 0.5/300/280 | YWDR0.6- 0.5/300/280 | YWDR1.0- 0.5/300/280 | YWDR1.5- 0.5/300/280 |
| Temp control accuracy | ℃ | PID±1℃ | |||||
| Power supply | / | 3PAC380V/480V 50HZ(3phase+Earth) | |||||
| Heat transfer medium | / | Thermal conductive oil | |||||
| Rated power | KW | 120 | 240 | 300 | 600 | 1000 | 1500 |
| Thermal efficiency | % | 98 | 98 | 98 | 98 | 98 | 98 |
| Design pressure | Mpa | 0.75 | 0.75 | 0.75 | 0.75 | 0.75 | 0.75 |
| Motor power | KW | 5.5 | 11.0 | 11.0*2 | 22.0*2 | 37.0*2 | 45.0*2 |
| Pump flow | m³/h | 34 | 50 | 50 | 100 | 160 | 200 |
| Pump head | m | 40 | 50 | 50 | 55 | 50 | 53 |
| Max. power consumption | KW | 127.5 | 251 | 322 | 622 | 1037 | 1545 |
| Alarm function | / | Pump reversal/Oil shortage/Overheating/Overload/Abnormal heating/Pressure to protect | |||||
| Connecting pipe size | inch | 2" | 3” | 3" | 4 " | 6” | 8” |
| Size(L×W×H) | mm | 2450*800*1900 | 2520*900*2100 | 2600*1000*2170 | 2800*1300*3000 | 3000*2200*3500 | 4200*3000*3800 |
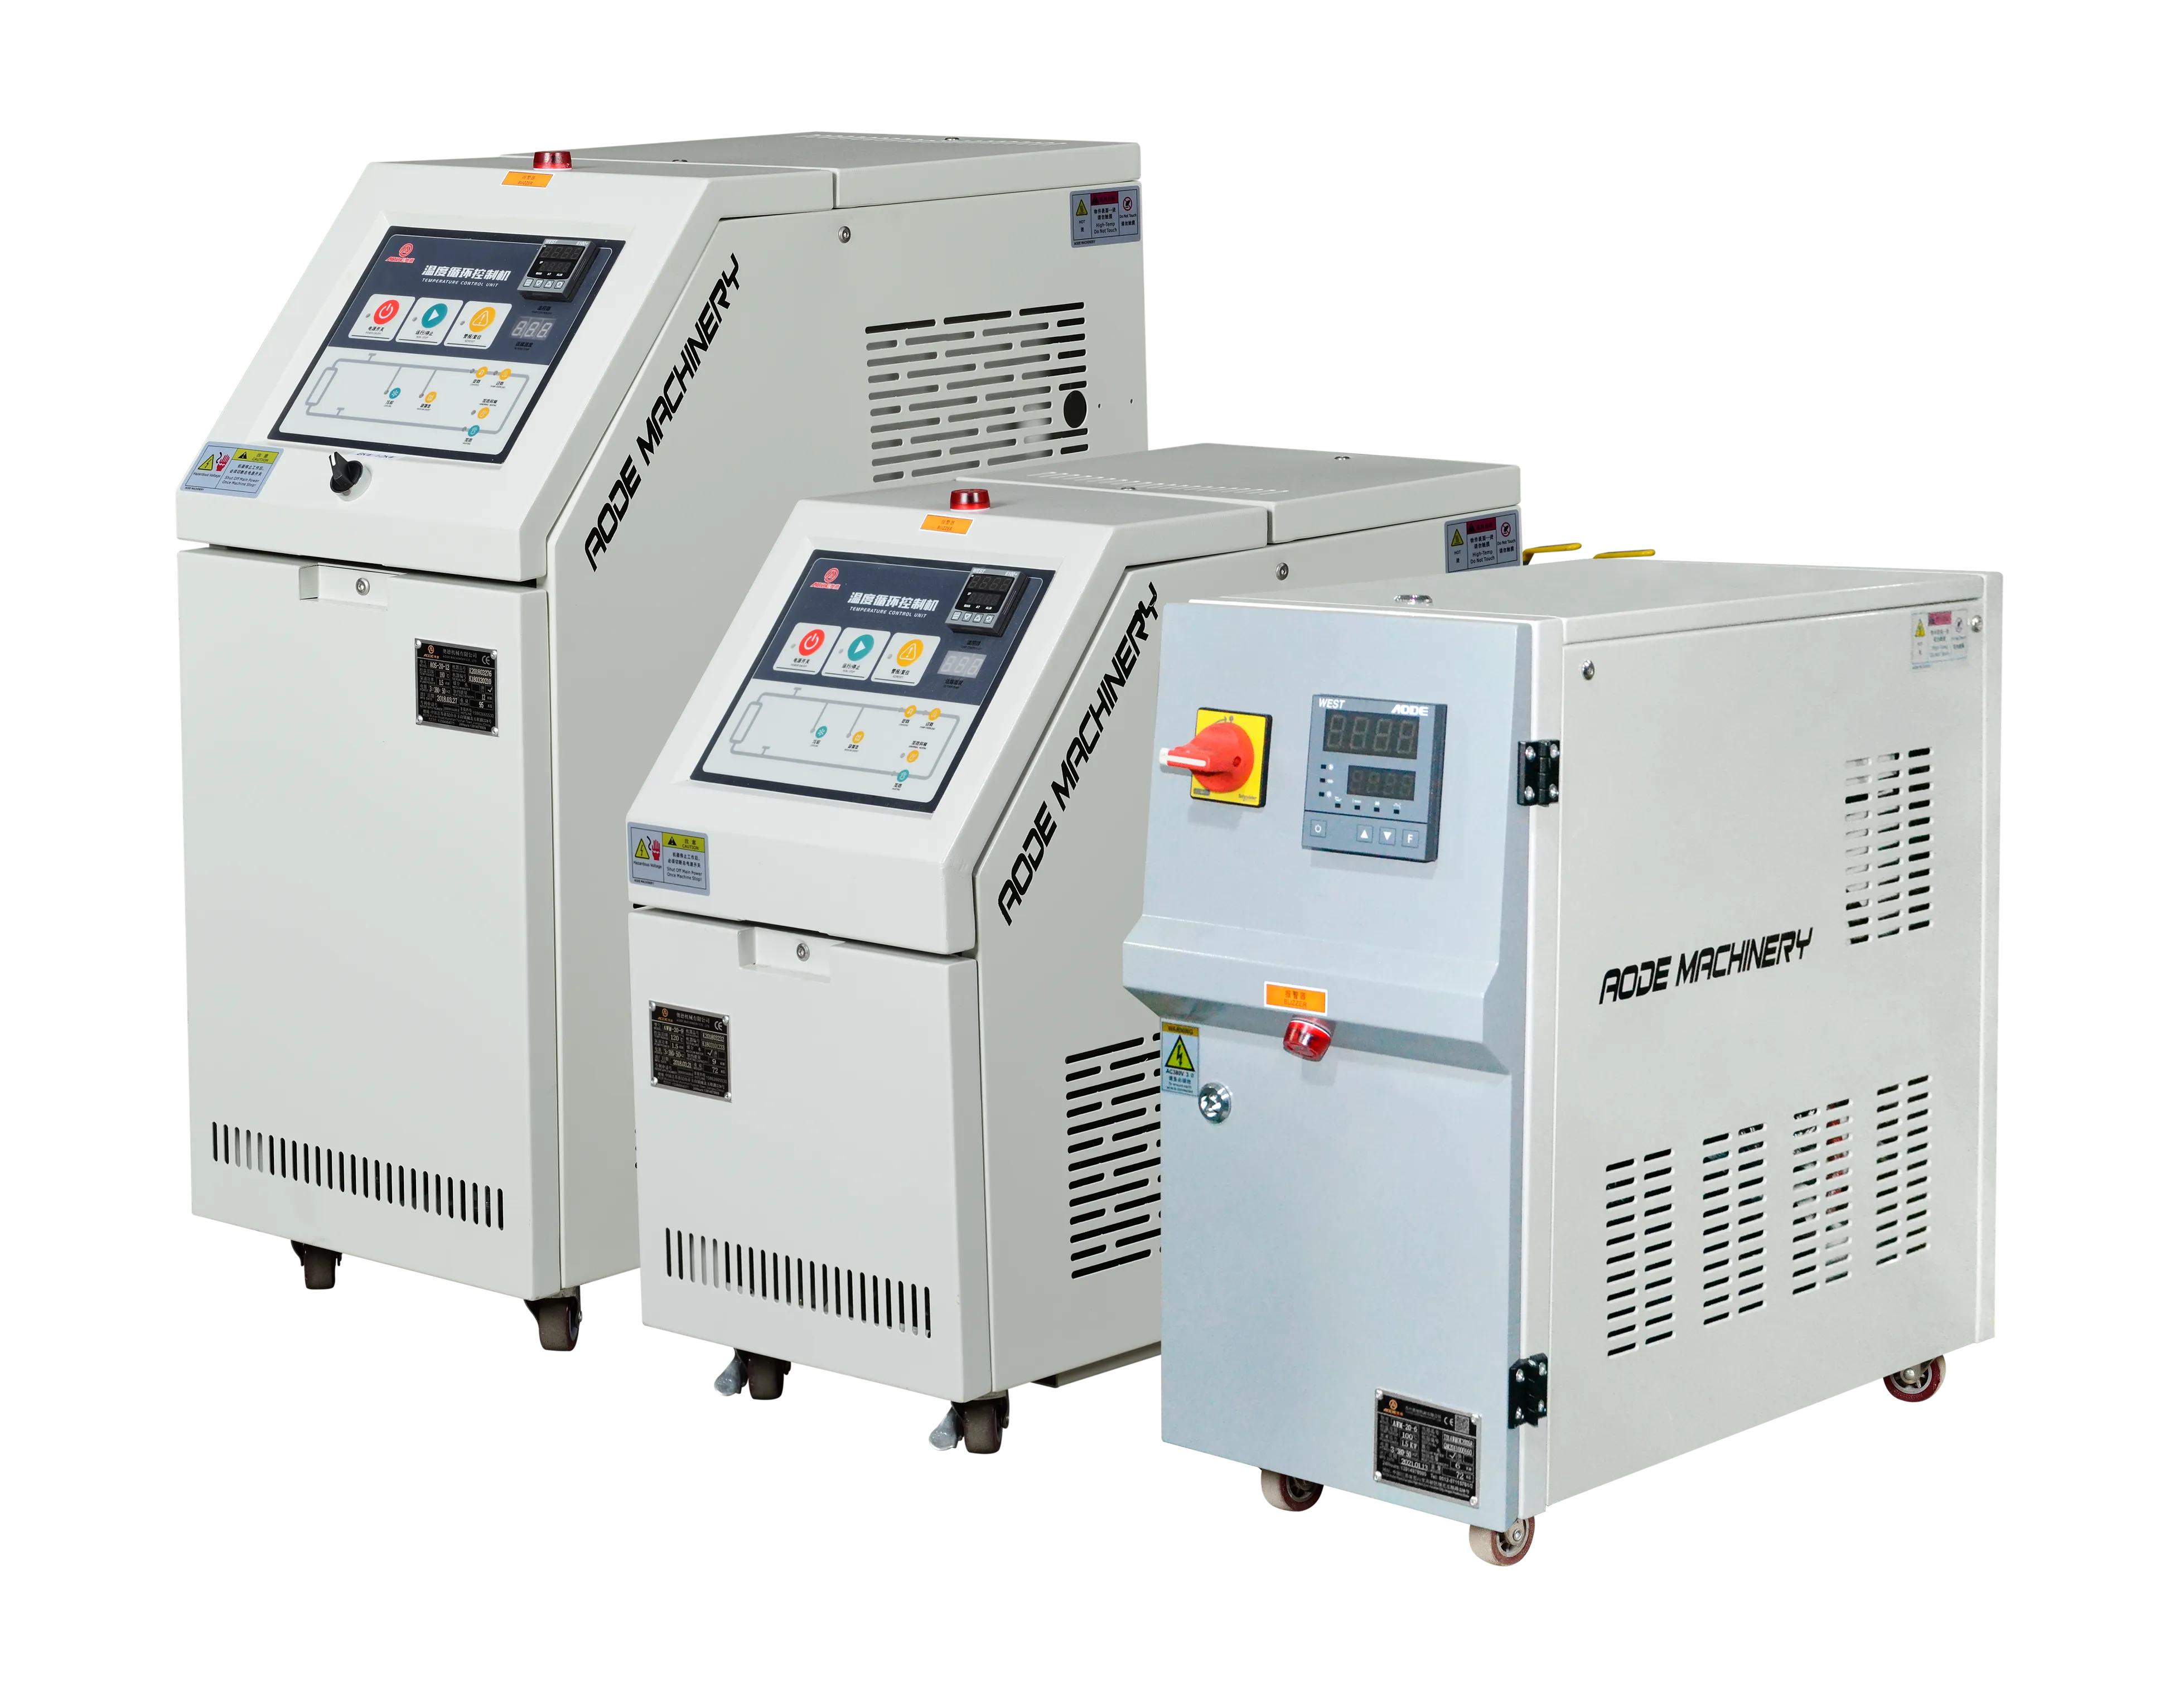
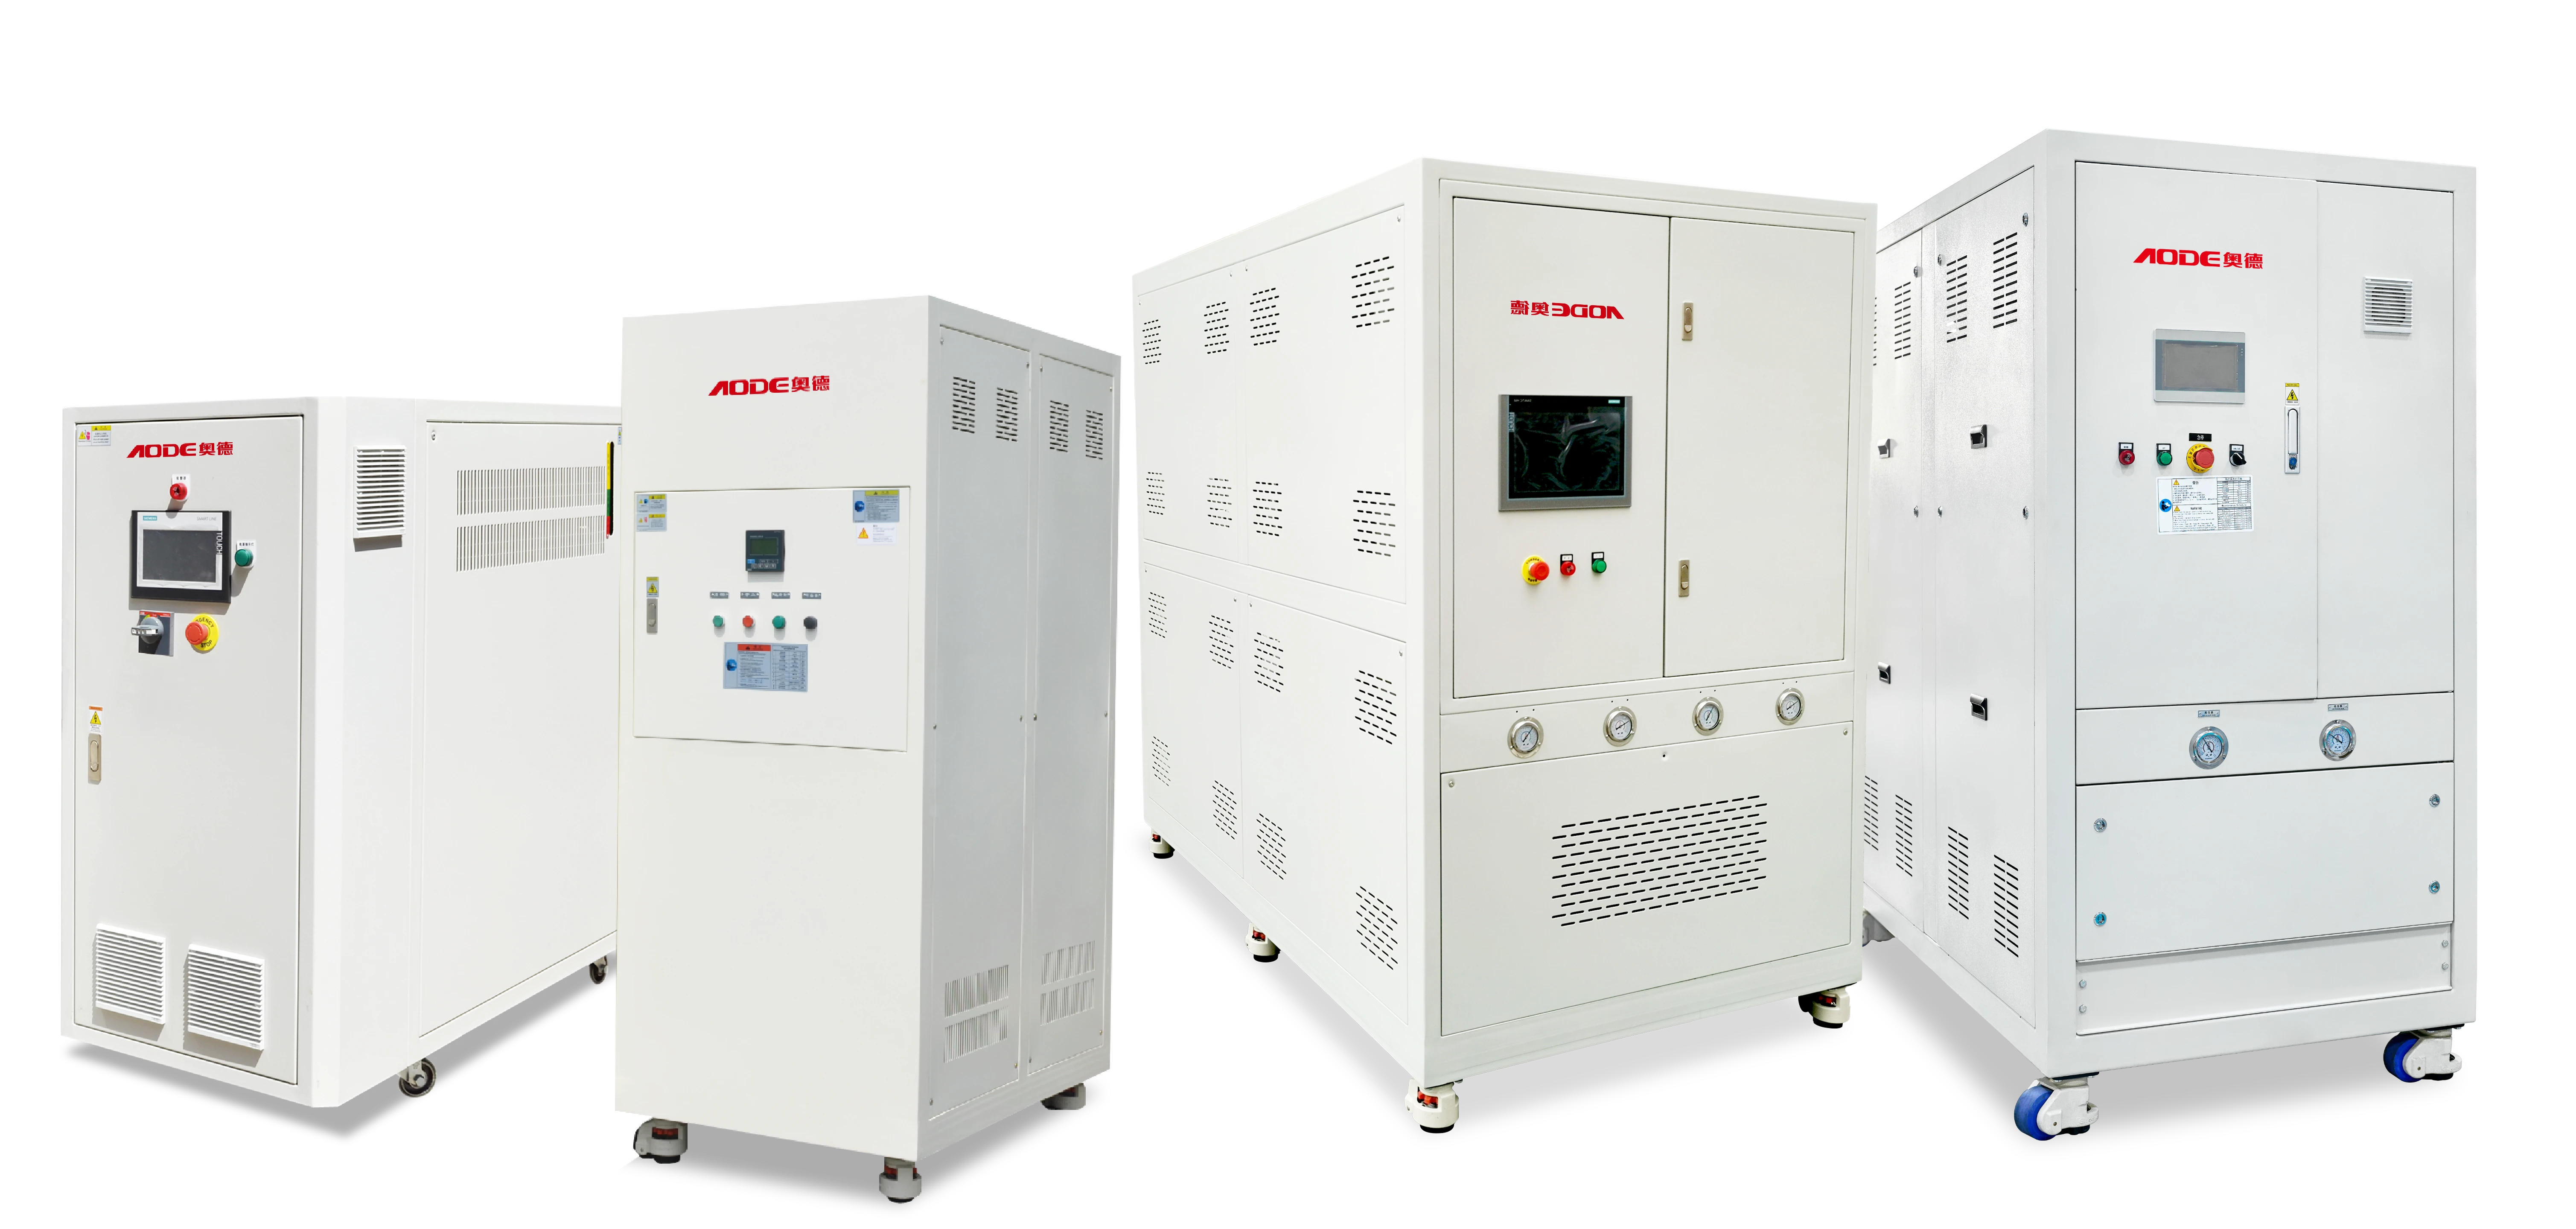
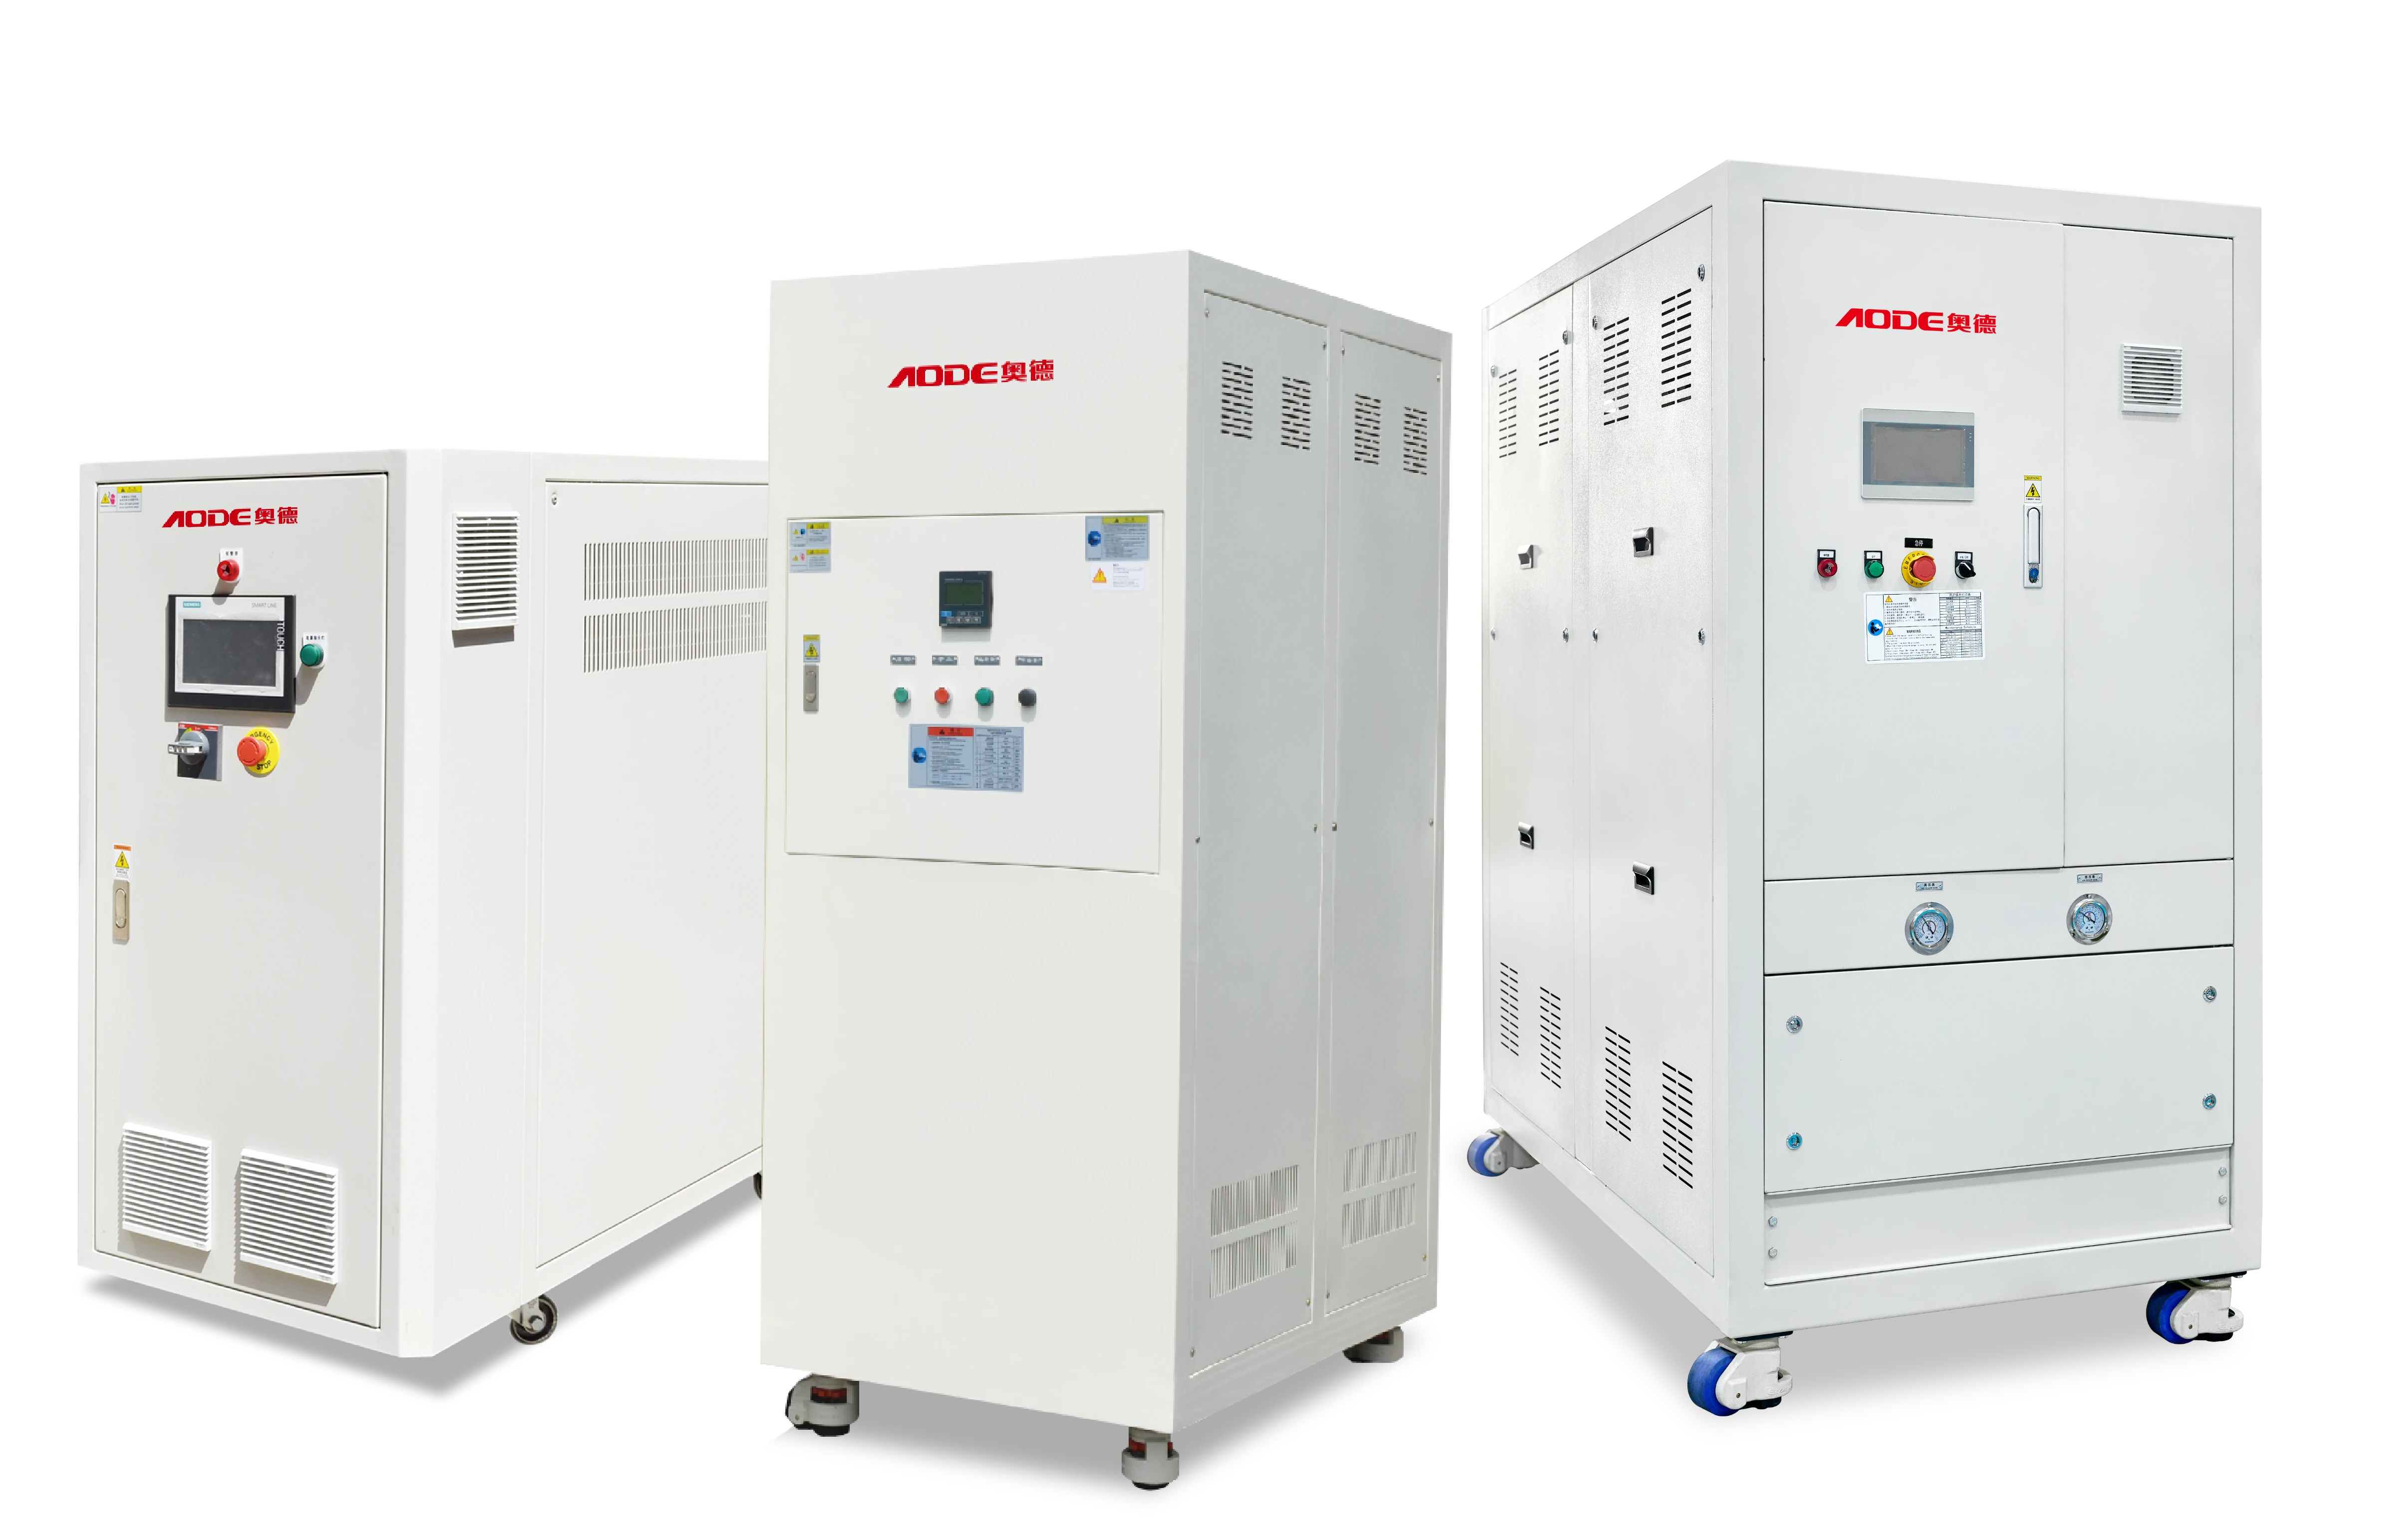
Heat Transfer Fluid System Related Products
FAQ
Can this heat transfer fluid system be integrated into automated production management systems?
Yes. This heat transfer fluid system supports optional RS485 communication functions for automated monitoring and management. The isolated electrical control box design helps protect electrical components, while intelligent fault display allows operators to monitor system status and simplify maintenance during long-term operation.
How efficient is the electrically heated organic heat transfer system during operation?
The electrically heated system achieves a thermal efficiency of up to 98% by directly converting electrical energy into heat transferred through thermal conductive oil circulation. Compared with conventional heating methods, this structure reduces heat loss during energy transfer and provides more stable temperature control for continuous production processes.
What safety features are included in this thermal fluid heating system?
This thermal fluid heating system integrates multiple safety protection functions, including pump reverse protection, oil shortage protection, overheating protection, overload protection, abnormal heating alarms, and pressure protection. Optional explosion-proof devices and pressure control designs help improve operational safety for high-temperature industrial environments.
How does this heat transfer fluid system support large-scale industrial heating requirements?
This industrial thermal oil heating system is designed with different circulation configurations to meet various heat transfer requirements. Depending on the model, the pump flow ranges from 6m³/h to 34m³/h, with pump heads from 28m to 50m, helping maintain sufficient thermal oil circulation for different equipment layouts and heating demands.
What makes an organic heat transfer fluid system suitable for high-temperature industrial processes?
An organic heat transfer fluid system provides indirect heating through circulating thermal oil, allowing heat transfer at high temperatures without direct flame heating or high-pressure steam requirements. The system can maintain uniform heat distribution and stable thermal performance, making it suitable for industries requiring precise temperature management and continuous operation.
What temperature range can this thermal fluid heating system achieve?
This industrial thermal oil heater supports a temperature control range of +45°C to +400°C and uses PID temperature control to maintain stable operation. The series provides heating capacities from 18kW to 96kW, with different configurations available according to thermal requirements, equipment size, and production conditions.